
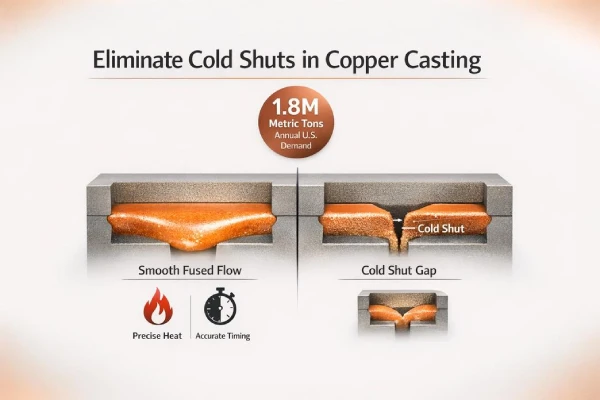
In high-volume copper casting production, cold shuts can result in significant losses. A single casting error can lead to production slowdowns and a buildup of scrap. For buyers of copper cast parts who demand strict tolerances and tighter delivery schedules, this can substantially increase production costs. However, copper cools rapidly, which impedes flow and makes it difficult for the molten metal to fuse properly. Without precise control over temperature and timing, profits will slip away from the mold.
The U.S. Geological Survey reports U.S. copper demand topping 1.8 million metric tons annually—proof this metal keeps industry humming. As ASM International notes, “Solidification control is central to casting integrity.”
This article provides an in-depth analysis of the causes of cold shuts in copper casting, covering technical challenges associated with sand casting, permanent mold casting, centrifugal casting, and ロストワックス鋳造. It also outlines practical strategies for temperature control, alloy properties, and simulation optimization to help foundries mitigate the risk of cold shuts.
Common Causes of Cold Shuts in Copper Casting
Cold shuts in copper casting are caused by subtle changes in heat, flow velocity, or alloy behavior during the actual casting process. Whether it is sand casting or centrifugal casting, every casting process has its vulnerabilities. The following section will analyze the causes of defects such as cold shuts in copper casting and how to avoid these issues through intelligent casting production.
Sand casting challenges in copper alloy pours
In copper sand casting, cold shut defects often occur when pouring highly thermally conductive copper alloys. This is because the sand mold rapidly draws heat away from the molten metal, causing the flow front to solidify prematurely and preventing proper fusion at the point where the metal flows converge.
In actual production, the main factors leading to cold shut defects in copper castings include:
- The high thermal conductivity of brass and bronze shortens the solidification window, reducing the fusion time at the convergence point.
- If the runner is designed too narrow, metal pressure decreases, making thin-walled areas more prone to premature solidification.
- Insufficient mold preheating, excessive moisture in the sand, and poor venting further exacerbate sudden temperature drops.
Higher thermal conductivity means a tighter time window. In its キャスティング制作, Supro MFG has optimized the pouring system and thermal simulation for copper alloy castings to ensure that the risk of cold shuts is minimized before the metal enters the mold cavity.
The following is a typical thermal comparison for copper castings:
合金の種類 | Pour Temp (°C) | Solidification Range (°C) | Conductivity (W/m·K) |
C360 Brass | 930–970 | 890–905 | 120 |
C932 Bronze | 1020–1050 | 950–990 | 60 |
純銅 | 1085–1150 | ~1085 | 390 |
Al Bronze | 1040–1080 | 1020–1040 | 35 |
Sn Bronze | 1000–1030 | 900–950 | 50 |
How low ductility in tellurium copper triggers splits
Although tellurium-copper alloys exhibit excellent machinability, their low ductility during solidification may lead to cold shut defects. The root cause lies in the fact that when this alloy is used in the copper casting process, the material’s properties within the high-temperature short-range region reduce its tensile strength and limit plastic deformation. When two metal streams converge, fusion is incomplete, and the presence of a surface oxide film leads to micro-separation at the joint. Ultimately, under the action of contraction stress, the micro-gap continues to widen, resulting in significant cracks in the copper 鋳造部品.
銅製 casting shops that prioritize speed over control, thin-walled electronic components are particularly susceptible to damage due to the mechanical behavior of this alloy. Complex geometries combined with rapid cooling can result in insufficient strength at the fusion line. Copper casting involves the fusion of the metal front under shrinkage stress. To produce higher-quality copper 鋳造部品, it is necessary to control overheating, balance gate flow rates, and ensure the purity of the melt composition.
Gating system design flaws in permanent mold casting
In permanent mold casting, heat dissipates from metal molds even faster than from sand molds. When cold shuts occur in copper castings, they are typically caused by defects in the ゲートシステム design. Excessively long horizontal runners and sharp bends cause turbulence in the molten metal, leading to a sudden drop in temperature before the cavity is filled; uneven 肉厚 results in varying cooling rates, and the absence of overflow channels causes gas bubbles to become trapped. If the flow velocity in the copper casting process is too low or the sprue deviates, the surface oxide film is prone to folding, while excessively high flow velocity exacerbates turbulence.
In copper casting, laminar flow is the golden rule, while turbulent flow can compromise fusion. Supro MFG uses simulation tools to optimize permanent mold pouring systems for casting projects, particularly in fields such as electrical connectors and heat transfer components where the clarity of the fusion line is critical.
Inconsistent mold temperature in centrifugal casting
Centrifugal casting incorporates a rotational step into the process; while this can increase the density of copper castings, it also rapidly exposes 熱処理 defects. When the mold temperature is unstable, subsurface cold shuts may form in the castings. This occurs because uneven preheating creates localized cold spots, causing the thin outer layer to solidify prematurely during rotation; subsequently, the molten metal coming into contact with the semi-solid layer fails to bond, resulting in interlayer separation.
Key control points for centrifugal copper casting include: maintaining preheating uniformity within ±15°C, ensuring stable rotational speed, maintaining a consistent metal feed rate, and controlling heat distribution. At Supro MFG, centrifugal copper casting projects utilize controlled preheating mapping technology to ensure uniform fusion throughout the wall thickness—a factor that is particularly critical for bushings and bearing sleeves, where structural integrity is paramount.
信頼できる中国の金属鋳造工場をお探しですか?
- 当社は、お客様の製品設計の最適化とコスト削減をお手伝いいたします。.
- 弊社では、高品質な 高品質で大量生産された鋳造品 部品。.
- 納期通りに納品し、さらなる販売機会を獲得することができます。.
- Supro MFGをご利用いただくと、さまざまなメリットがあります 金属鋳造 サービス。.
5 Hidden Causes of Cold Shuts in Copper Casting
The risk of cold shuts in the copper casting process can be attributed to five underlying causes. Even minor deviations in control parameters can accumulate rapidly; once the flow of molten metal, mold temperature, and alloy composition deviate from equilibrium, cold shuts can form unnoticed, disrupting the solidification and shaping of the casting.
Improper wall thickness in gravity casting
In gravity casting, uneven wall thickness design can interfere with the solidification and flow of the copper casting. When the 金型設計 is unbalanced, thin-walled areas cool too quickly, while thick-walled areas retain heat for longer. During pouring, the molten metal front splits and forms an oxide layer, ultimately leading to reduced fusion strength. Once the copper casting has cooled, defects and hidden bonding gaps become clearly visible.
For copper castings with sharp transition surfaces, even the slightest variation in thickness can alter the thermal gradient. In copper 合金鋳物, this mismatch hinders proper fusion and directly leads to cold shuts.
Slow fill speeds during lost wax casting
In lost-wax casting, if the filling rate is too slow, the molten metal will lose heat before the mold cavity is filled. Major signs of failure in copper casting include poor spout design, excessively narrow runners, and excessive back pressure.
When the molten flow stagnates, the leading edges of the two streams meet in a cold area, and the resulting oxide layer prevents proper fusion. In the production of investment-style copper castings, adjusting the casting process speed allows for maintaining good fluidity while rapidly reducing cold shuts.
Low thermal conductivity in phosphor bronze pours
Phosphor bronze has relatively low thermal conductivity, which causes heat to diffuse slowly during the casting process and makes it prone to the formation of localized hot spots. Uneven temperature distribution during pouring can lead to uneven solidification during cooling. Therefore, co-casting copper alloys and bronze requires stricter thermal control. Otherwise, isolated cooling zones may form within the copper casting, preventing proper fusion at the leading edge of the molten pool.
Inadequate mold preheating and heat treatment gaps
Cold shuts can typically be traced to improper mold preheating during copper casting. If the initial mold temperature is too low, the surface metal will cool rapidly. Combined with an uneven post-casting heat treatment cycle, this will cause a rapid decline in the quality of the copper casting. To avoid this problem, the solutions are:
- Raise the mold temperature to a level consistent with the alloy’s melting point range.
- Ensure the temperature is stable before pouring the molten copper.
- Maintain consistent thermal management throughout the pouring process.
- Perform consistent heat treatment after pouring.
Overlooking ASTM specifications for material certification
ASTM standards are often overlooked in the copper casting process, specifically regarding unverified material certifications, lax quality control, and inconsistent material properties. Fluctuations in chemical composition can affect the copper’s fluidity, ductility, and 耐食性. This alters solidification behavior and increases the risk of cold shuts in copper castings.
Partnering with a meticulous copper casting foundry like Supro MFG helps ensure the use of certified alloys, controlled casting parameters, and more rigorous inspection processes. For teams that prioritize the reliability of metal castings, Supro MFG ensures the predictability of copper castings—which is key to preventing cold shuts.
Reverse the Chill: Copper Casting Pouring Temperature Secrets
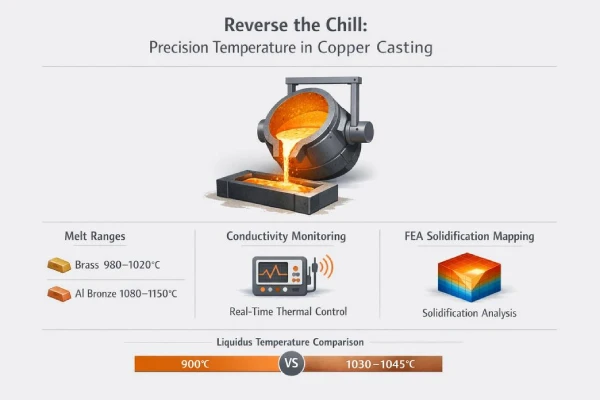
Precise temperature control is essential for successful copper casting. From brass to bronze, once the molten metal begins to flow, each copper alloy reacts differently. In modern foundries, precise temperature control translates to fewer defects and tighter tolerances.
Optimal melt ranges for brass and aluminum bronze
In copper casting, the optimal melting temperature range ensures smooth melt flow without causing the loss of alloying elements. For brass and bronze, strict temperature control helps maintain the alloy’s chemical composition and final strength. As a professional copper casting foundry in China, Supro MFG typically adjusts the following parameters based on the actual mold geometry to consistently ensure the stable performance of cast 部品。.
Different types of brass (Cu-Zn series) are affected by their composition in different ways. For 60/40 brass (which has a higher zinc content), the liquidus temperature is lower. Lead-containing brass, on the other hand, has a narrower melting temperature range and offers better machinability. When controlling the temperature range, pouring at too high a temperature can lead to zinc oxidation, while pouring at too low a temperature can cause gate defects in thin-walled copper castings.
For aluminum bronze (Cu-Al series), the aluminum content (8–12%) causes the liquidus line to shift upward and makes the alloy susceptible to oxidation, so the furnace atmosphere must be carefully controlled. The following table compares common copper alloys:
合金の種類 | Liquidus (°C) | Recommended Pour Temp (°C) | Oxidation Risk Level |
60/40 Brass | 900 | 980–1020 | 中 |
Leaded Brass | 890 | 950–1000 | Medium-High |
9% Al Bronze | 1030 | 1080–1120 | 高い |
11% Al Bronze | 1045 | 1100–1150 | 高い |
Leveraging electrical conductivity data to dial in heat
During the copper casting process, changes in electrical conductivity reflect both composition and temperature. A change in conductivity indicates an anomaly within the molten metal: elevated conductivity may indicate high copper purity and low alloy content, while a sudden drop in conductivity may indicate overheating or contamination. Stable conductivity readings indicate that the pouring temperature is well controlled.
Many copper casting foundries follow these standard operating procedures:
1) Measure the baseline conductivity of the target alloy.
2) Monitor readings during the holding phase in the furnace.
3) Adjust the burner or induction input in small increments.
The 2025 International Copper Study Group noted that energy efficiency and thermal monitoring are “key cost drivers in non-ferrous foundry competitiveness.”
“Advanced process monitoring, including thermal and conductivity tracking, is accelerating yield improvement across global copper-based casting operations.” — International Copper Study Group, 2025 outlook
For foundries specializing in large-scale copper casting, electrical conductivity data plays a critical role. Supro MFG has successfully used this method to stabilize the production processes for both small- and large-batch copper 鋳造部品.
Using FEA analysis to predict solidification patterns
Modern FEA tools integrate science into everyday casting operations. In copper casting, predicting solidification patterns helps reduce shrinkage and porosity before the metal enters the mold. By inputting the thermal conductivity and latent heat of the copper alloy, along with mold boundary conditions, solidification patterns can be predicted to identify hot spots and areas of high shrinkage. When optimizing the copper casting process, modifying wall thicknesses and adjusting risers and gating channels can effectively reduce cold shuts and porosity.
For any copper casting production, digital simulation can shorten the trial-and-error phase. Supro MFG combines actual furnace data with FEA results to ensure that cast copper parts are dimensionally accurate and structurally sound.
Supro-Mfgへのお問い合わせ
Eliminating cold shuts in copper casting requires systematic control of alloy properties, mold temperature, and gating system design. From 砂型鋳造 to centrifugal casting, optimizing parameters through electrical conductivity monitoring and FEA simulation can significantly improve casting density.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina