
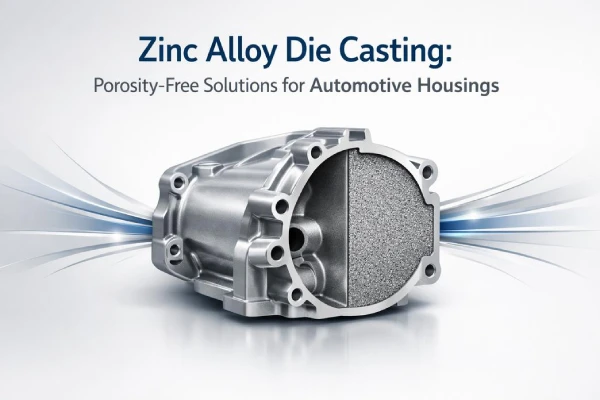
Due to its excellent fluidity and dimensional stability, zinc alloy die casting has become the preferred solution for automotive, electronic, and industrial housing components. However, porosity remains a key challenge that threatens the structural density, sealing performance, and plating quality of zinc alloy die cast parts.
Overcoming porosity issues in zinc alloy die casting requires a shift from experience-driven to data-driven precision control. This article provides an in-depth analysis of the three primary causes of porosity: entrapped air caused by fluctuations in injection pressure, shrinkage cavities resulting from uncontrolled mold thermal equilibrium, and flow turbulence caused by improper wall thickness design. To address these technical challenges in ダイカスト, we have developed a standardized solution that encompasses injection parameter optimization, precise thermal management, Mold Flow analysis, and rigorous post-processing. Using comparative experimental data, we demonstrate how scientific control of mold temperature and cooling rates can significantly improve the density and surface finish of zinc alloy die cast 製品。.
In response to the extremely stringent tightness requirements for housings in high-precision industries such as the automotive sector, Supro MFG has further optimized its gate design and quality assurance protocols for high-volume production, ensuring that every batch of die cast parts meets rigorous mechanical performance and assembly tolerance standards. Highly reliable zinc alloy die cast parts are not merely metal components; they embody a commitment to performance and serve as the cornerstone for enhancing overall system efficiency and reducing costs.
Why are housings made by zinc alloy die casting so prone to porosity defects?
Zinc alloy die casting is the preferred choice for housing components due to its excellent fluidity and dimensional stability. However, porosity remains a major challenge that threatens the structural density and plating quality of zinc alloy die cast parts. The following section provides an in-depth analysis of the three key factors that cause porosity.
Gas entrainment caused by fluctuations in injection pressure
In zinc alloy ダイカスト, stable injection pressure ensures the proper flow of molten metal; any fluctuations in pressure can lead to a cascade of problems. During the die casting process, molten zinc alloy is injected into the mold cavity at high speed. A sudden drop in pressure within the cavity disrupts the filling process, preventing gases from escaping smoothly and resulting in entrapped air. Inside the zinc alloy ダイカスト金型 cavity, the entrapped air mixes with the molten zinc, forming internal voids as the gas becomes trapped. When the metal solidifies, these voids manifest as porosity.
The presence of porosity has a significant impact on the performance of zinc alloy die 鋳造部品. This includes reduced strength in zinc die cast parts, the formation of leakage paths in thin-walled shells, and the appearance of surface bubbling after machining or electroplating.
To address this issue, Supro MFG’s process engineers monitor pressure curves in real time during zinc alloy die casting production. By strictly controlling the flow characteristics of the zinc alloy and the operating status of the die casting machine, they effectively minimize porosity, helping customers avoid scrap waste.
The Effect of Insufficient Cooling Rate on Porosity Formation
In the production of zinc alloy die cast parts, any imbalance in the cooling rate leads to porosity issues. In hot spots, heat dissipates slowly, delaying the solidification process. Internal gases are trapped in thick-walled sections before they can escape, resulting in noticeable shrinkage cavities and porosity. More problematic still, localized overheating of the die 鋳型 extends cycle times, while excessive cooling induces internal stress—both extremes cause the risk of porosity in zinc alloy die cast parts to skyrocket. Controlling heat flow is essential to maintaining the density and fatigue resistance of castings from the ground up.
According to a 2025 outlook from the North American Die Casting Association, improved thermal control systems in 亜鉛ダイカスト operations are directly linked to lower internal defect rates and better structural reliability.
Therefore, Supro MFG meticulously calibrates the temperature control zones and cooling channels in every zinc alloy die casting solution. Consistent cooling enables zinc alloy die castings to develop a denser grain structure, thereby reducing hidden porosity.
Design errors in wall thickness and draft angle
Even the most sophisticated zinc alloy die casting production line can result in scrap products due to poor design; design details directly determine whether castings can be produced without porosity. Excessive 肉厚 is a common pitfall: it slows down core cooling, increases shrinkage stress, and makes it easier for internal voids to form. In zinc alloy die cast parts, if there is no smooth transition at points where wall thickness changes abruptly, the flow of molten metal becomes turbulent, trapping gas during filling and resulting in porosity.
Draft angles are equally critical. If the draft angle on zinc alloy die cast parts is insufficient, the parts are difficult to remove from the mold, the surface is prone to tearing, and external forces can damage the casting’s structure; if the draft angle is too steep, dimensions deviate from design specifications, resulting in poor fit during assembly. More subtle issues include sharp corners, improper venting system layout, and geometric defects overlooked during the initial CAD design phase.
A sound zinc alloy die casting design must adhere to the physical principles of metal flow—ensuring that molten zinc flows smoothly, fills the mold uniformly, and cools in a controlled manner. A comprehensive review of wall thickness transitions, draft angles, and the overall mold design prior to mold opening is essential to ensure that the properties of the zinc alloy and the process parameters work in harmony rather than conflict with one another. Only by addressing design flaws at the source can porosity issues in zinc alloy die casting products be effectively controlled.
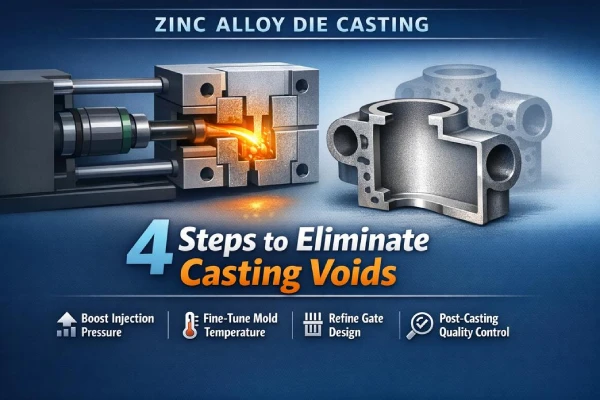
4-Step Process for Eliminating Porosity in Zinc Alloy Die Castings
As a die casting manufacturer with years of industry experience, Supro MFG has developed a standardized solution to address the challenge of porosity in zinc alloy die casting. This approach encompasses the optimization of injection parameters, thermal management, mold runner design, and rigorous post-processing. By leveraging advanced mold flow analysis technology to optimize gate layout, we not only effectively suppress the formation of porosity but also ensure that housing components deliver outstanding performance in both leak testing and precision machining. Below are the four key steps for delivering high-quality zinc alloy die cast products.
Step 1: Increase injection pressure and optimize filling time
亜鉛中 alloy die casting, maintaining stable injection pressure and a controlled filling time ensures that the molten metal fully fills the mold cavity before solidification. Key process control measures include calibrating the die casting machine, setting an appropriate pressure ramp curve, ensuring proper lubrication of the injection sleeve, and maintaining a stable flow rate. These measures help minimize gas entrapment and improve the filling efficiency of zinc alloy die cast parts.
Applying a gradual pressure increase during the zinc alloy die casting process can prevent turbulence in the molten metal, shorten filling time, and prevent flash formation, while also allowing for monitoring of changes in density and tensile strength. As a professional manufacturer of zinc alloy die cast parts in China, Supro MFG optimizes the pressure curve to ensure smooth and steady flow of the molten zinc alloy, thereby reducing porosity defects and ensuring consistent part weight.
Step 2: Precise Control of Mold Temperature and Cooling Rate
Thermal management is key to controlling porosity in the zinc alloy die casting process. A symmetrical layout of the mold heating channels and cooling passages ensures uniform heat dissipation. The smaller the temperature imbalance, the fewer defects in the castings—uniform cooling refines the grain structure, improving the hardness and surface finish of zinc alloy die cast parts.
Balanced mold temperature and cooling rates allow for precise control of the solidification process in zinc alloy die casting. The following are empirical comparison data showing the relationship between mold temperature, cooling rates, and the porosity and surface finish of zinc alloy die cast parts:
zinc alloy die casting partsMold Temp (°C) | Cooling Rate (°C/s) | Porosity (%) | Surface Finish (Ra μm) |
160 | 25 | 1.8 | 1.6 |
180 | 20 | 0.9 | 1.2 |
200 | 15 | 0.7 | 1.1 |
Step 3: Optimizing Gate Design and Number of Cavities
Proper gate design ensures smooth metal flow in zinc alloy die casting. The key lies in balancing the runner system, controlling gate thickness, arranging vent channels, and optimizing the number of cavities and pressure distribution. This enhances the quality consistency and production efficiency of zinc alloy die cast parts.
Too many cavities can lead to insufficient molten metal supply, while too few can waste die casting machine cycle time. Adjusting the mold design ensures stable zinc alloy die casting operations while extending mold service life. Supro MFG conducts flow simulation data analysis prior to mold machining, which reduces rework and ensures the repeatability of the zinc alloy die 鋳造工程.
Step 4: Post-die casting Finishing, Machining, and Leak Testing
Even perfectly formed zinc alloy die cast parts require a comprehensive post-processing procedure. The process includes:
- Trimming flash and sprue scrap
- Precision machining
- Thread cutting
- Surface finishing
- Pressure leak testing
- Dimensional scanning to ensure dimensional accuracy
- Visual inspection to ensure surface integrity
- Final inspection to strengthen quality control
Before each batch of zinc alloy die cast parts leaves the factory, they must undergo rigorous sealing and assembly inspections. To ensure reliable performance, zinc alloy parts must meet requirements for smooth edges and consistent tolerances.
信頼できる中国の金属鋳造工場をお探しですか?
- 当社は、お客様の製品設計の最適化とコスト削減をお手伝いいたします。.
- 弊社では、高品質な 高品質で大量生産された鋳造品 部品。.
- 納期通りに納品し、さらなる販売機会を獲得することができます。.
- Supro MFGをご利用いただくと、さまざまなメリットがあります 金属鋳造 サービス。.
Key Processes for Porosity-Free Zinc Alloy die cast Automotive Housings
Given the automotive industry’s extremely stringent density requirements for zinc alloy die cast housings, the manufacturing process must ensure end-to-end quality control, from mold design to final product inspection. As a die casting manufacturer with deep expertise in the automotive parts supply chain, Supro MFG strictly adheres to the IATF 16949 quality standard. By integrating advanced automated machining, deburring solutions, and X-ray non-destructive testing technology, we ensure that every zinc die cast part delivers exceptional sealing performance and structural strength.
Gate Design and Control of Wall Thickness Variations
High-density zinc alloy die cast parts rely on proper gate design and consistent wall thickness control. Regarding gate design, during the mold design phase, the flow balance of the runner system must be optimized, and flow simulation should be used to predict potential gas entrapment locations. During the injection phase, injection speed and pressure must be adjusted, and melt temperature controlled to ensure uniform filling of the zinc melt. For zinc alloy die cast parts, any area with poor venting can become a source of porosity.
Wall thickness control is equally critical. The dimensions of the ribs in the structural areas of zinc alloy die cast parts should be kept uniform, and abrupt changes in wall thickness should be avoided to minimize shrinkage defects and internal stresses. Critical sealing surfaces must maintain coaxiality, and appropriate draft angles should be provided to facilitate smooth demolding of the zinc alloy die cast 部品。.
As professional manufacturers of zinc alloy die cast parts, Supro MFG’s engineers meticulously optimize every gate and vent design to eliminate porosity defects, ensuring that the castings meet stringent sealing and assembly requirements.
Post-casting Machining and Deburring Plan
High-quality zinc alloy die cast products earn customer trust, and the use of precision machining and scientific deburring methods ensures the surface quality and dimensional accuracy of die cast parts.
During the finishing stage, automated equipment is used to remove flash from zinc alloy die cast parts, and edge quality is inspected prior to secondary machining. During CNC finishing, the focus is on controlling the flatness of mounting surfaces and the perpendicularity of bearing seats. Surface pretreatment of zinc alloy die cast parts prepares them for painting and electroplating, while also verifying the absence of microcracks resulting from post-casting machining.
As a professional manufacturer of zinc alloy die cast parts in China, Supro MFG integrates automated processes into the キャスティング制作 to ensure consistent batch quality and earn long-term customer trust.
Sampling Plans for Quality Assurance in Mass Production
Automotive mass production lines operate at a fast pace, and the inspection of zinc alloy die cast parts must keep pace with this efficiency. Supro MFG employs cavity pressure charts in its process control to monitor weight and density in real time. During the final verification stage, X-ray inspection is used to detect hidden porosity, and acceptance criteria are established based on tensile properties. A material certificate is issued for each batch of zinc alloy die cast parts, and each individual casting is assigned a unique code for traceability.
A 2025 McKinsey automotive manufacturing update noted that lightweight metal components, including 亜鉛ダイカスト鋳物, remain central to cost control and electrification efficiency goals. Therefore, zinc alloy die cast parts are not merely metal components; they are a testament to performance.
Supro-Mfgへのお問い合わせ
In summary, porosity defects in zinc alloy die cast housings primarily stem from fluctuations in injection pressure, imbalanced cooling rates, and design flaws. By optimizing injection parameters, precisely controlling mold temperature, and refining gate and cavity designs—combined with post-casting precision machining and rigorous inspection—this technical challenge in zinc alloy die cast parts can be effectively overcome.
For high-end applications such as the automotive industry, adhering to stringent quality standards and implementing end-to-end control of zinc alloy die cast parts, coupled with scientific processes and inspection methods, enables the stable mass production of high-quality, porosity-free zinc alloy die castings that meet the industry’s rigorous requirements.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina