
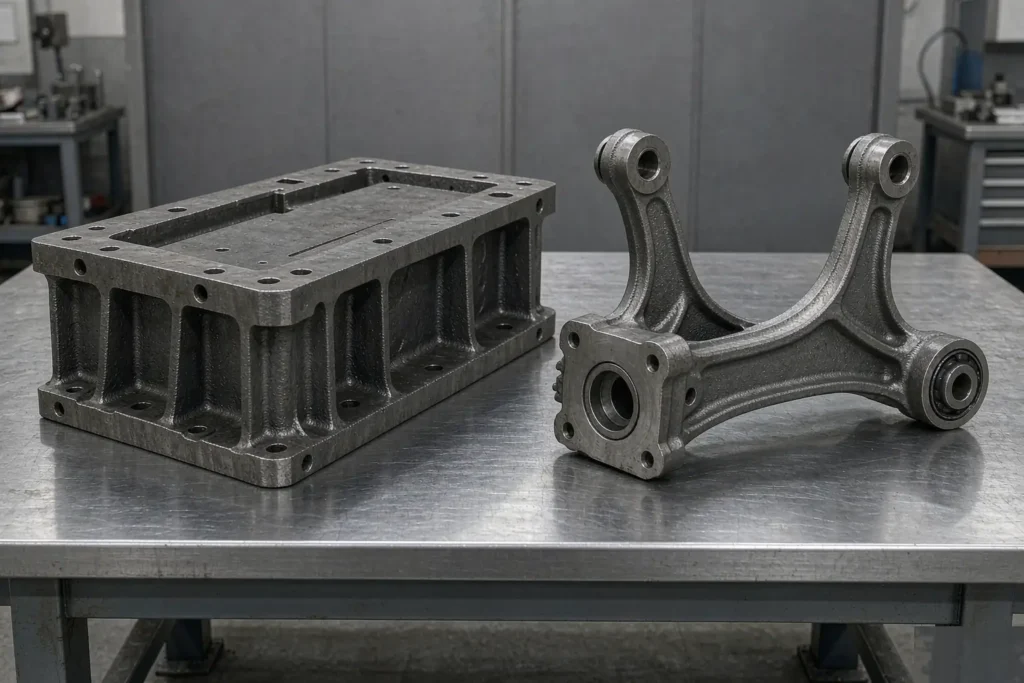
Few material calls cost as much as gray iron vs ductile iron. Choose gray iron for a part that takes shock load and you ship a component that can crack in service; choose ductile iron for a static machine base and you pay a 15–30% premium for toughness and ductility the part will never use. This guide puts both families side by side with real ASTM numbers, shop-floor machining data, and a six-question checklist you can run in ten minutes.
Everything below is drawn from the two standards that govern any gray iron vs ductile iron specification — ASTM A48 for gray iron, ASTM A536 and ISO 1083 for ductile iron — plus the cost and cycle-time records from our own foundry and machine shop. Where a value depends on section thickness or heat treatment, we say so instead of quoting a single number. For independent metallurgical background, the 米国鋳造学会 and the Ductile Iron Society both publish free technical material.
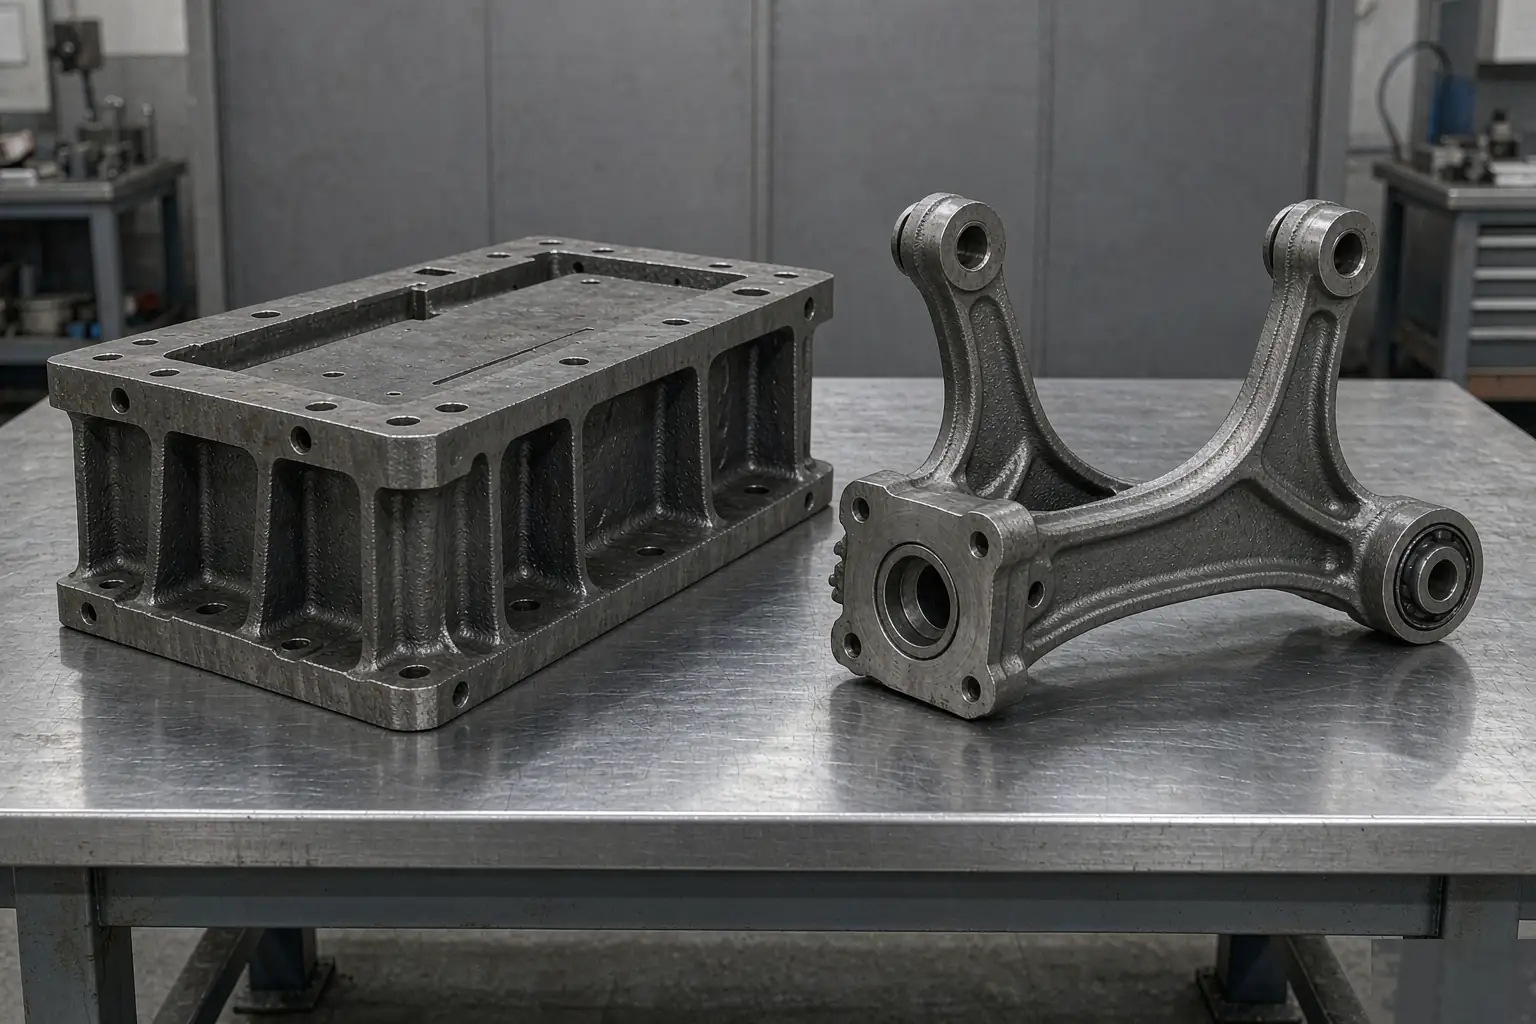
Gray Iron vs Ductile Iron: What Actually Differs
Both alloys sit in the same Fe-C-Si family: roughly 2.5–4.0% carbon and 1.0–3.0% silicon, both poured into sand molds, both machined on the same equipment with the same carbide grades. The entire performance gap comes from one thing — the shape of the graphite that precipitates during solidification.
- Gray iron. Carbon precipitates as interconnected flakes (ASTM A247 Type A is the usual target). The fracture face looks gray, which is where the name comes from.
- Ductile iron. A small magnesium addition — typically 0.03–0.05% residual Mg after nodulizing — forces the graphite to grow as spheres instead of flakes.
In gray iron every flake tip behaves like a pre-existing crack. Load concentrates at those tips, and the metal fails with almost no plastic deformation. In ductile iron a sphere has no tip, so the surrounding matrix can deform and work-harden before it tears. That single geometric difference explains every property gap in the tables below. If you want the metallurgical background in more depth, our article on sand casting microstructures walks through how cooling rate sets the structure you end up with.
Why flake graphite behaves like a crack
Graphite itself has almost no strength. A flake is therefore an internal notch with a tip radius close to atomic dimensions — a crack the casting is born with. The practical consequence is that gray iron has no measurable yield point and essentially 0% elongation. Designers do not use yield data for it at all; they use tensile strength for tension cases and a compressive strength that runs roughly 3–4 times higher than tensile. A Class 30 iron at 214 MPa tensile will carry something in the order of 750 MPa in compression. That asymmetry is exactly why gray iron dominates machine bases, housings and counterweights, where the load is nearly all compressive.
What nodularity really means
Nodularity is the percentage of graphite particles that are genuinely spheroidal, judged against the ASTM A247 comparison charts. Most foundry specifications call for ≥80%; safety-critical automotive and wind components often hold ≥90% with a nodule count above 100 per mm². Below 80% you lose elongation and fatigue life quickly — a 65-45-12 heat that nodulizes at 70% will not reliably deliver 12% elongation.
Nodules also degrade in heavy sections. Slow cooling produces chunky graphite, exploded nodules and nodule flotation, all of which cut properties in the very areas you least expect. If your part has a 60 mm or 100 mm wall, agree on chills, chemistry and gating with the foundry before the drawing is frozen — the conversation belongs in mold and pattern design, not after first article.
Mechanical Properties Side by Side
Read the grade numbers carefully, because the two families do not use the same scale. An ASTM A48 class number is the minimum tensile strength in ksi. An ASTM A536 grade is tensile ksi / yield ksi / percent elongation. So “Class 40” and “80-55-06” cannot be compared by number alone. In practice, the gray iron vs ductile iron decision is rarely a straight strength ranking — it is a question of whether you need yield and elongation at all.
| 素材 | Tensile (MPa) | Yield (MPa) | 伸び | Typical HB | Typical part |
|---|---|---|---|---|---|
| Gray iron A48 Class 20 | 152 | n/a (brittle) | ~0% | 150–190 | Counterweights, light covers |
| Gray iron A48 Class 30 | 214 | n/a (brittle) | ~0% | 180–230 | Pump bodies, machine bases |
| Gray iron A48 Class 40 | 276 | n/a (brittle) | ~0% | 200–260 | Engine blocks, brake drums |
| Ductile A536 60-40-18 | 414 | 276 | 18% | 149–187 | Pipe fittings, valve bodies |
| Ductile A536 65-45-12 | 448 | 310 | 12% | 156–217 | Suspension arms, hubs |
| Ductile A536 80-55-06 | 552 | 379 | 6% | 187–255 | Crankshafts, gears |
| Ductile A536 100-70-03 | 689 | 483 | 3% | 241–302 | Wear plates, heavy brackets |
Whichever way the gray iron vs ductile iron decision goes, hardness is where prints most often go wrong. Hardness figures for gray iron are indicative shop ranges, not values specified by ASTM A48 — the standard governs tensile strength on a separately cast test bar only. If your print calls out a hardness band, state the location on the casting where it must be measured.
Where Each Wins: An Application Map
The fastest way to shortlist is to look at what similar parts actually use. The gray iron vs ductile iron split by application is remarkably consistent across industries, because it tracks load case far more closely than it tracks cost.
| 用途 | Pick | 理由 |
|---|---|---|
| Machine tool bed, column | Gray Class 30–35 | Damping capacity plus high compressive stiffness |
| Brake rotor, brake drum | Gray Class 35–40 | Thermal conductivity around 48 W/m·K, good wear |
| Manhole cover, counterweight | Gray Class 20–25 | Lowest cost per kg, almost no tensile demand |
| Crankshaft, camshaft | Ductile 80-55-06 | Fatigue strength under rotating bending |
| Steering knuckle, control arm | Ductile 65-45-12 | Impact absorption, ductility at low temperature |
| Pressure valve body, pipe fitting | Ductile 60-40-18 / 65-45-12 | Elongation and pressure tightness, weld repair possible |
| Wind turbine hub, rotor support | Ductile EN-GJS-400-18-LT | Charpy energy ≥12 J at -20 °C |
| Hydraulic cylinder, gearbox housing | Ductile 80-55-06 / 100-70-03 | Yield strength under sustained internal pressure |
Sector work makes the gray iron vs ductile iron pattern easy to see, because the same component type tends to land on the same alloy everywhere. Our 自動車用鋳物 そして valve castings programs run both alloys on the same lines, and the iron casting service page lists the grades we pour routinely.
Heat, Vibration and Machining Behaviour
Three physical properties drive the gray iron vs ductile iron choice more often than tensile strength does, and buyers rarely see them on a material spec sheet. If your part is a housing, a bed or a rotating friction component, read this section before the tables above.
- Thermal conductivity. Gray iron runs about 46–52 W/m·K because the flake network carries heat; ductile iron sits near 36–38 W/m·K. That 25–30% advantage is why brake rotors and engine blocks stay gray.
- Damping capacity. The same flake network dissipates vibrational energy. Gray iron damps several times better than ductile iron and roughly an order of magnitude better than steel. Machine tool builders still specify it for beds and columns for precisely this reason.
- Machinability. Graphite lubricates the cut and breaks the chip. Gray iron Class 30–35 with carbide tooling typically runs 250–350 m/min; pearlitic 80-55-06 at a comparable hardness runs 150–220 m/min.
Cutting speed and cycle time
That speed gap of roughly 60–65% translates directly into cycle time: expect 40–60% longer machining on ductile iron for the same material removal. Grade selection inside the ductile family matters just as much. Ferritic 60-40-18 machines far more easily than pearlitic 100-70-03, so if a part is machined heavily and does not need the strength, specify the ferritic grade and accept the lower numbers. Our comparison of CNC加工と鋳造の比較 covers how to plan stock allowance around this, and the CNC machining service page shows the equipment we run cast iron on.

Castability, Section Sensitivity and Shrinkage
Feeding behaviour is the least discussed part of the gray iron vs ductile iron comparison, and it is where schedules slip. Start with carbon equivalent, the single number foundries use to predict solidification behaviour: CE = %C + (%Si + %P) / 3.
- Gray iron example. C 3.30, Si 2.00, P 0.05 → CE = 3.98. Sitting near the eutectic, graphite precipitates during solidification and expands, offsetting most of the liquid shrinkage. Gray iron is largely self-feeding, and many sections need little or no riser.
- Ductile iron example. C 3.60, Si 2.50, P 0.03 → CE = 4.44. Better fluidity for thin walls, but magnesium shifts solidification toward a pasty mode, so ductile iron needs deliberate feeding: risers, chills, or a riserless design backed by a very rigid mold.
Section sensitivity is the trap in nearly every gray iron vs ductile iron specification. ASTM A48 classes are defined on a separately cast test bar, not on your casting. A Class 40 bar at 30 mm diameter shows 276 MPa; the same iron in a 100 mm wall can test nearer Class 25–30, around 170–210 MPa, because slow cooling coarsens the graphite. Thin walls under about 6 mm swing the other way and chill into free carbides that destroy machinability. Always give the foundry the critical wall thickness together with the grade — the two are inseparable. Our guides to casting tolerances そして 一般的な鋳造欠陥 expand on how geometry drives both.
What the Cost Difference Actually Buys
On a per-kilogram basis, ductile iron typically runs 1.15–1.30 times gray iron. The premium is not arbitrary; it covers four identifiable things that every gray iron vs ductile iron quote should be able to itemise.
- Nodulizing and inoculation. FeSiMg alloy plus a controlled ladle or tundish treatment, with magnesium fade managed against a tight time window.
- Tighter base chemistry. The iron must be low in sulfur before magnesium is added, which usually means pre-treatment and stricter charge control.
- Heat treatment. Ductile iron is routinely ferritizing-annealed or normalized; gray iron usually ships as-cast or with stress relief only. See our heat treatment guide for the cycles involved.
- Inspection. Nodularity per ASTM A247, tensile testing per heat, and ultrasonic or magnetic particle inspection on critical sections.
Weighed against a field failure, the premium is small. Weighed against a 5,000-piece run of a static housing, it is not — and it compounds with slower machining. If the part never sees tensile shock, gray iron is the honest economic answer. Our マナコストの内訳 shows where each cost line sits in a real quote.
How to Choose: A Six-Question Checklist
Run these in order. A single “ductile” answer on questions 2, 4 or 5 usually settles the gray iron vs ductile iron debate regardless of what the other five say.
- What is the dominant load? Compression plus vibration points to gray iron. Tension, bending or impact points to ductile iron.
- Is there a shock or low-temperature requirement? Any Charpy value or -20 °C condition means ductile, normally a ferritic grade such as EN-GJS-400-18-LT.
- What is the critical wall thickness? Below 6 mm or above 60 mm, discuss chills and chemistry with the foundry before locking the grade.
- Does the part hold pressure? Yes means ductile iron, without much argument.
- How much machining is involved? Heavy material removal on a static part makes gray iron win twice — cheaper material and shorter cycle time.
- What is the annual volume? At 50 pieces, tooling and process setup dominate. At 50,000, the per-kilogram delta does.
If you are still weighing alloys rather than iron grades, start with our 金属鋳造ガイド for the wider process map, then the casting alloy selection framework for a full comparison across aluminum, steel and iron.
よくある質問
Can I switch a gray iron part to ductile iron without redrawing it?
Geometrically usually yes, but the tooling does not transfer, because the gray iron vs ductile iron feeding layouts are not interchangeable. Ductile iron flows better, so thin sections fill more easily, yet it shrinks differently and needs a different feeding layout. Budget for revised gating and risering, and expect a new first-article round.
Is one of them heavier?
Barely. Both sit around 7.1–7.2 g/cm³, so a 10 kg part differs by a few tens of grams at most. Weight is not a deciding factor in the gray iron vs ductile iron comparison.
Does ductile iron resist corrosion better?
No. Both are ferrous and both rust at similar rates in the same environment. Protection comes from coating or plating rather than from the grade — see our surface finishing options.
Can either one be welded for repair?
Both are difficult. Ferritic ductile iron can be repaired with preheat around 300–400 °C, a nickel-based filler and post-weld stress relief. Gray iron repair welding is generally avoided because the heat-affected zone cracks. Design iron castings for replacement rather than weld repair.
Which one holds tighter tolerances?
Neither — in the gray iron vs ductile iron comparison, tolerance is set by the molding process and the pattern, not the alloy. Sand-cast gray and sand-cast ductile share the same ISO 8062 tolerance bands. Shell molding or a better mold will move the number; changing the alloy will not.
For a low-volume prototype run, which way does the gray iron vs ductile iron choice go?
For a prototype, the gray iron vs ductile iron call is really about what the sample has to prove. Start with gray iron if the prototype is only proving geometry and fit. It is cheaper per kilogram, faster to machine, and delivers parts sooner. Move to ductile iron for the validation build if that build is meant to prove strength or impact performance — testing a gray iron prototype will not tell you anything about how the ductile production part behaves. Our 金属試作鋳造サービス runs both so the comparison can be made on the same tooling.
Is compacted graphite iron the middle option?
Yes. CGI grows vermicular graphite, lands between the two on strength, and keeps more of gray iron’s thermal conductivity. It is the standard answer when you need more than gray iron but cannot accept ductile iron’s lower conductivity and slower machining — and it costs more than both, with a notably narrower process window.
There is no universal winner in the gray iron vs ductile iron debate. There is only the load case, the wall thickness, the volume and the machining route. Send us the drawing and the service conditions, and we will tell you which one belongs on the print — including when the answer is neither.
*Data referenced from ASTM A48 / A536 / A247, ISO 1083, AFS and Ductile Iron Society publications, and Supro MFG shop-floor records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina