
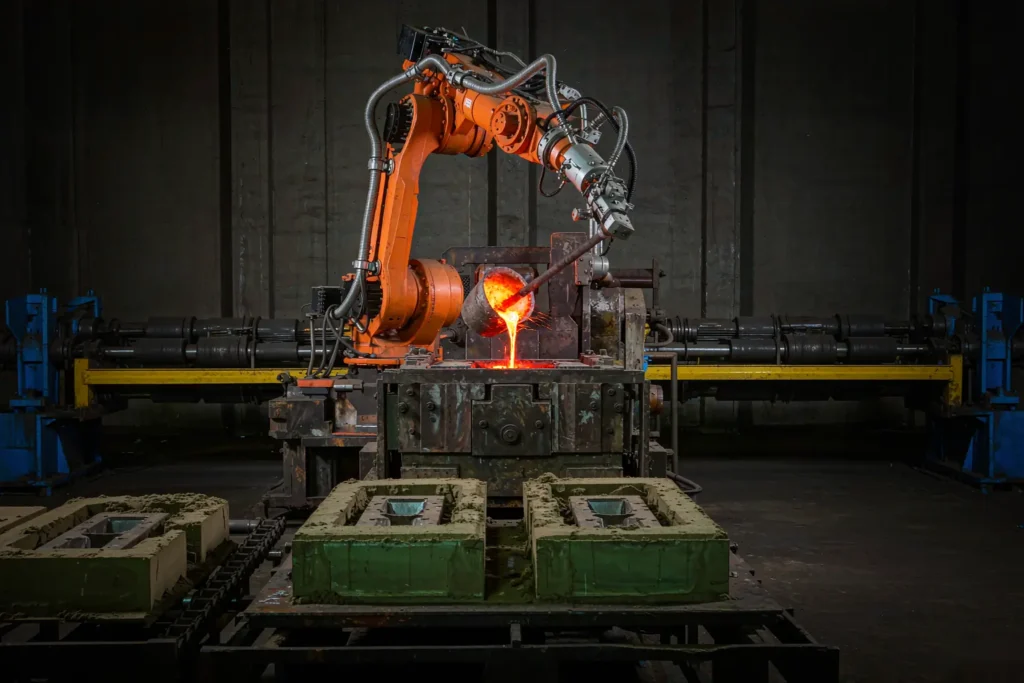
When a casting supplier mentions its robotic pouring cell or automated molding line in a quote, most buyers nod politely and move on to the price. That is a missed signal. Foundry automation is one of the strongest predictors of whether your quoted price holds across a multi-year program, how stable your part-to-part consistency will be, and how much schedule buffer the shop really needs behind your delivery date.
This guide explains where foundry automation actually lands inside a casting plant, what each layer changes for the numbers on your quote, and which questions to ask before you award. It draws on shop-floor records, AFS そして NADCA industry publications, and IFR robot installation data — with real cost math you can re-run against your own program. If you are new to the process side first, start with our complete metal casting guide.
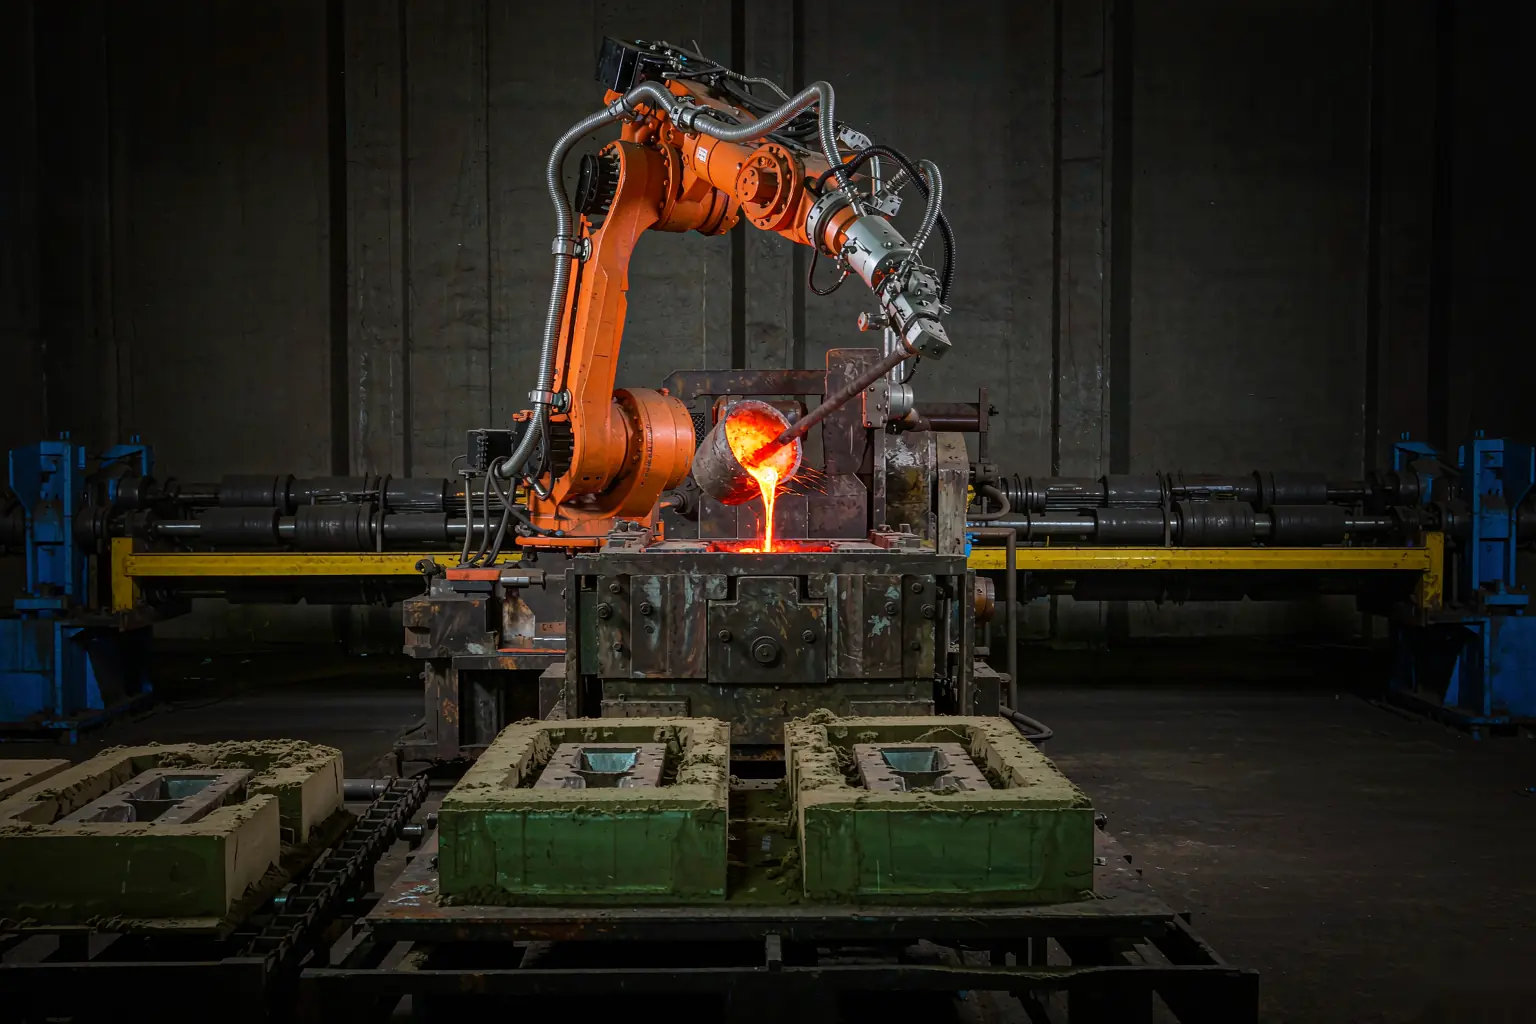
Where Foundry Automation Lands First in a Casting Plant
Automation arrives where repetition is high and variation is expensive. A jobbing 砂型鋳造 shop rarely automates everything at once; it invests layer by layer, and each layer has a distinct effect on what you receive.
| Plant layer | What it replaces | Typical rate or gain | What the buyer sees |
|---|---|---|---|
| Melting & charge | Manual bucket charging, guesswork alloys | Weighed charge to ±0.5%; auto spectral verification per heat | Chemistry certificates that actually match every heat |
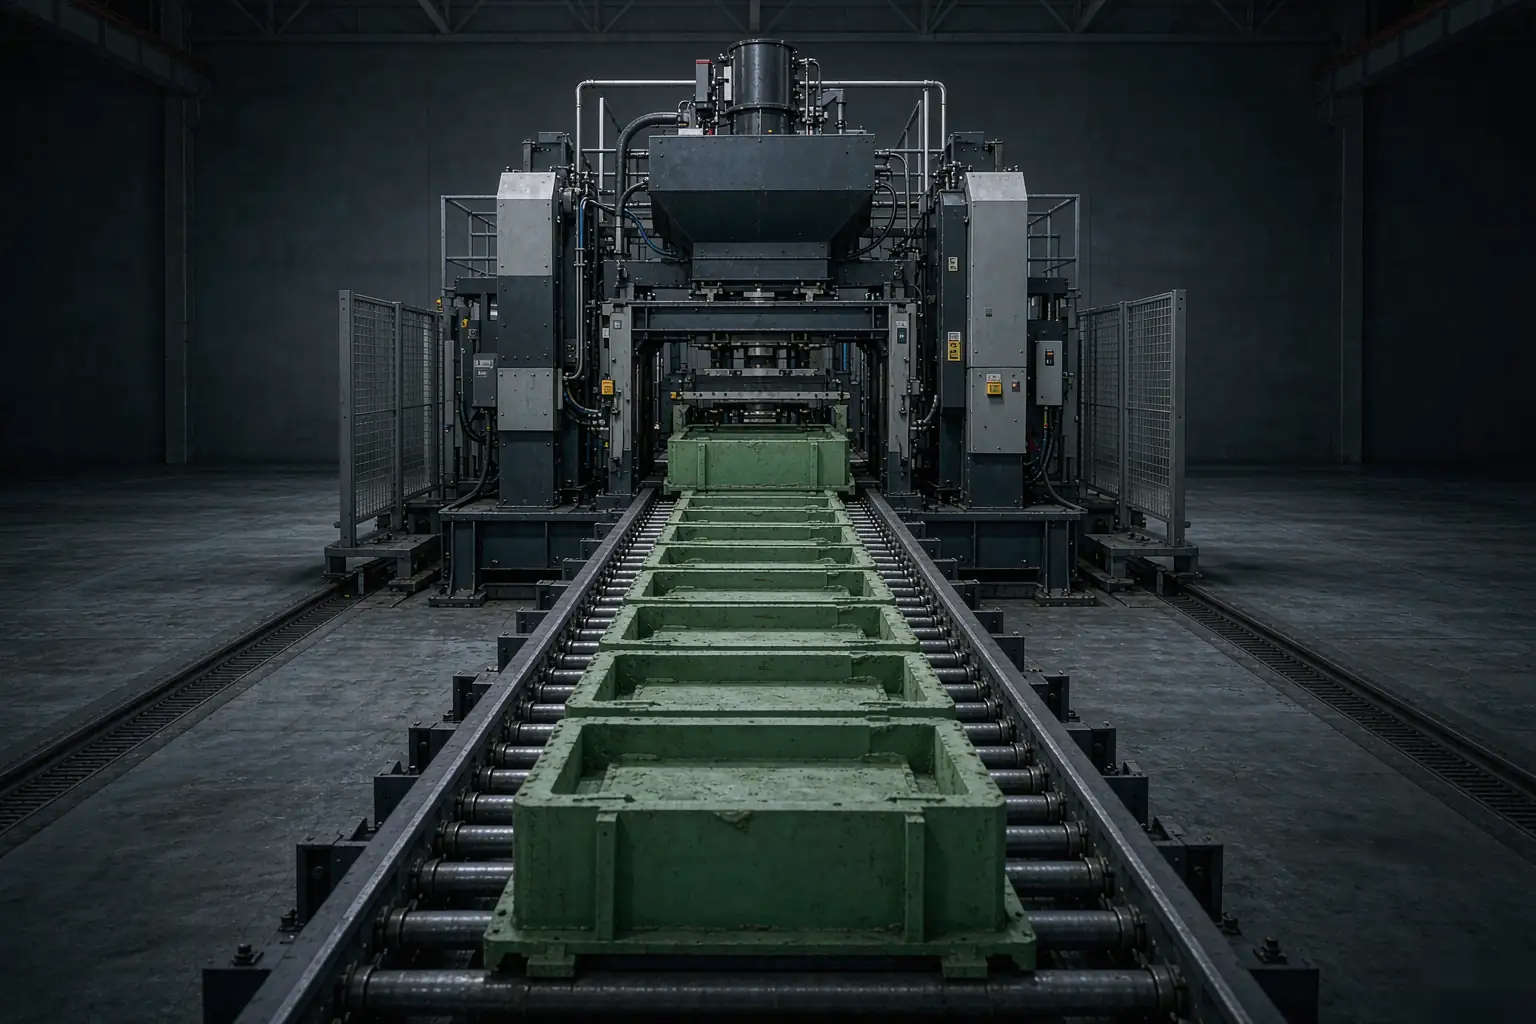
| Molding | Two-person floor molding, hand ramming | Flaskless line 120–200 molds/h vs. 10–15 molds/h manual | Shorter lead times, tighter dimensional scatter, lower MOQ |
| Core setting | Hand-placed cores in open molds | Pick-and-place with vision check before close | Fewer core-shift and veil defects on cored parts |
| Pouring | Hand ladle, visual judgment of stream | Robotic ladle with laser level control, ±5 °C | Steady misrun/porosity scrap rates instead of shifts |
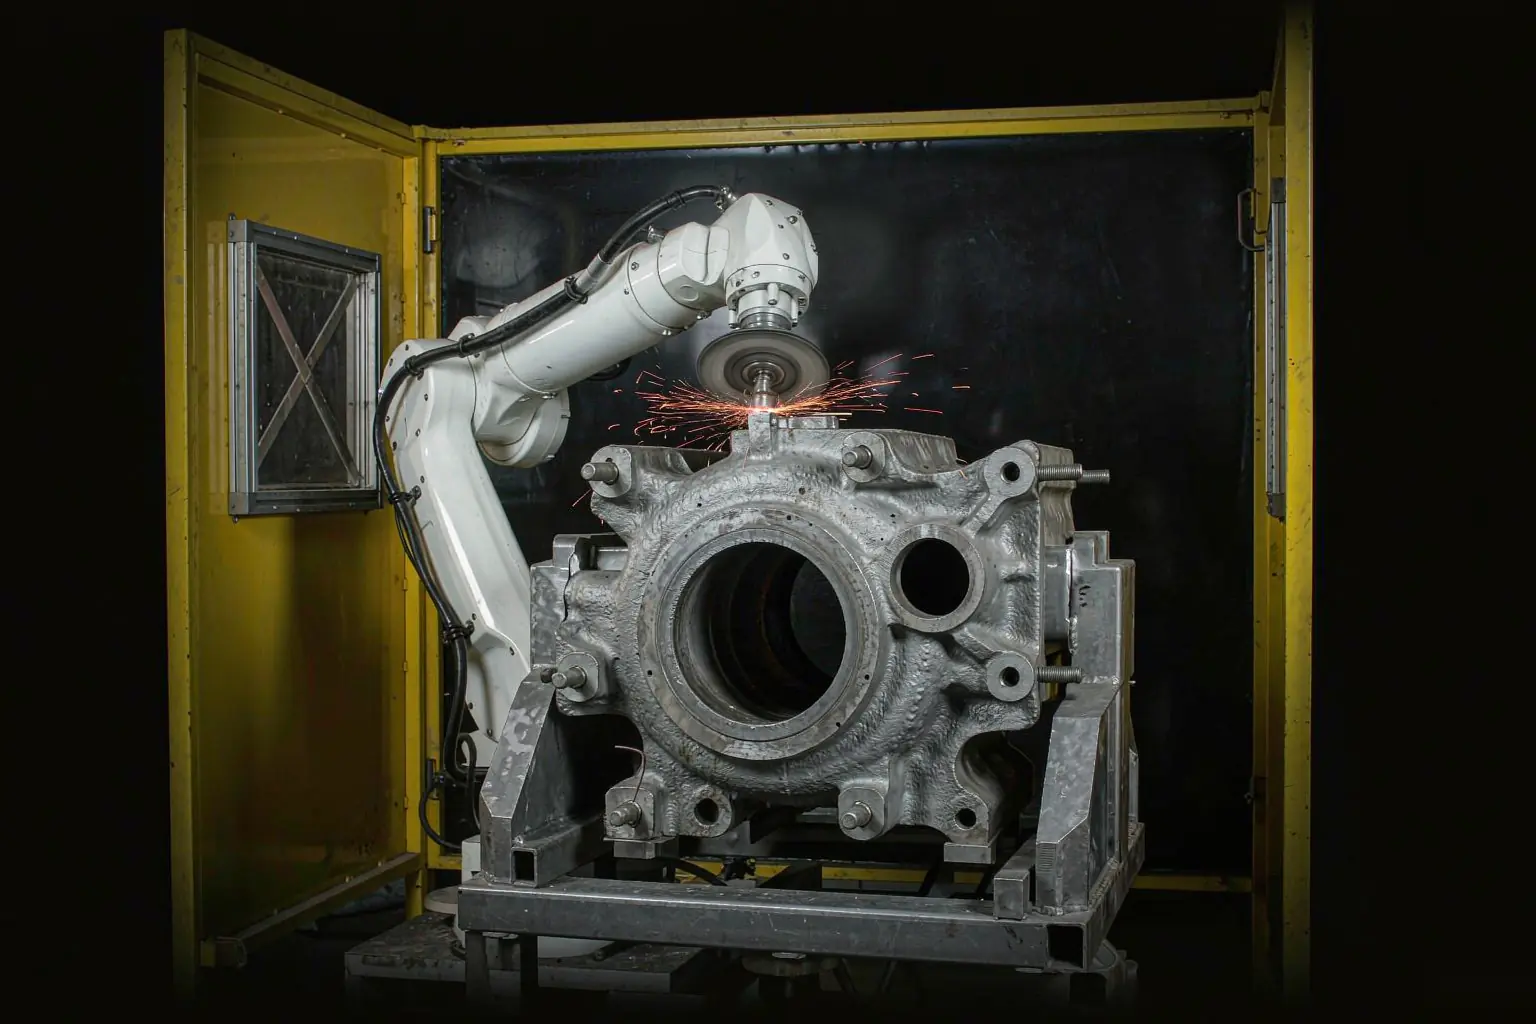
| Finishing | Manual grinders, chisels, files | Robotic grinding cells with force control | Uniform flash removal, stable finishing cost |
| Inspection | Sampling by a trained eye | Automated vision gating, digital defect maps | Escape rates you can track shipment by shipment |
Two structural notes. First, ダイカスト そして aluminum die casting are inherently machine processes — automation there is the machine itself — so this discussion matters most when you buy sand, shell or ロストワックス鋳造. Second, high-pressure lines and squeeze casting cells automate pouring under pressure as a condition of the process, not as an upgrade.
What Foundry Automation Does to Your Unit Price
In manual sand casting, finishing labor alone often runs 30–40% of the part cost — every casting is ground, chiseled and blended by hand, and every hour of that labor sits in your quote as a wage-plus-overhead line. That is the first place automation attacks. Work through the arithmetic of a typical robotic finishing cell:
- Installed cost. A two-station robotic grinding cell with force control, part fixturing and safety enclosure: about $185,000 installed.
- Labor recovered. It replaces roughly two full-time finishing operators across two shifts. At $52,000 fully burdened per operator-year, that is $104,000 per year.
- Consumables and rework. Consistent wheel pressure and angle cut abrasive waste and over-grind rework by about $12,000 per year.
That is $116,000 of annual recovery against $185,000 of capex — a 1.6-year payback, and thereafter the finishing cost of your part stops rising with local wages. This is why a shop that has absorbed foundry automation into finishing can hold a multi-year price on a 2,000+ part-per-year program, while a fully manual competitor must re-price at every wage round. For the full anatomy of where labor, material and energy sit in a casting price, see our マナコストの内訳.
Consistency You Can Measure: Pouring and Molding
The second dividend of foundry automation is statistical, and it shows up in your inspection reports rather than your invoice. A hand ladle pours with a temperature spread of roughly ±15 °C depending on operator, transfer distance and ladle skin; a robotic ladle with laser melt-level control holds ±5 °C. Pour too cold and you invite misruns and cold shuts; pour too hot and you invite gas porosity, sand burn-on and mold erosion. Between operators, shifts and Monday mornings, that spread is exactly where week-to-week quality drift comes from.
Run the scrap arithmetic for a mid-size ductile iron housing at 18 kg net weight and 55% yield — 32.7 kg poured per good part. If pour-related defects cost $18.50 in metal, energy and conversion for each scrapped part, then on a 12,000-part-per-year program, cutting pour-related scrap from 6% to 2.5% avoids 420 scrap events and saves the foundry about $7,770 per year — on one part number. Multiply across a line running dozens of part numbers and you can see why automated pouring spreads beyond the giant automotive plants.
Molding automation works the same way in the dimensional column. Machine-squeezed molds deliver uniform mold hardness mold after mold, so the casting wall you measure in October matches the one you measured in March instead of drifting with whoever rammed the mold that day. When your drawing calls ISO 8062-3 grades, a stable process is what makes those tolerances repeatable — our 鋳造公差ガイド explains which grades assume machine molding rather than hand ramming, and our 鋳造検査方法 guide shows how to verify the claim on real shipments.
The data layer: traceability comes with the machine
One underrated dividend of foundry automation is the record it produces. A manually poured mold exists for a few minutes and leaves no trace; an automated line logs mold number, squeeze pressure, core presence and pour temperature for every single mold. When a defect escapes to your receiving dock six weeks later, that log converts a heated argument into a two-minute lookup: which molds, which heat, which shift, and whether the process ran inside its window. Practically, this is what makes a credible casting quality agreement enforceable — acceptance criteria tied to heat numbers and mold identity rather than opinion — and it is the cheapest containment you will ever buy. Ask for a sample log with your first article report; a shop running real foundry automation will hand one over as routine.
Lead Time, Lot Size and the Real MOQ Behind It
Capacity is the third dividend. A flaskless automated molding line closes 120–200 molds per hour; a skilled two-person floor crew closes 10–15. Pattern changeover on the automated line is a 20–40 minute swap; on the floor it is an afternoon of flasks, jackets and ram-up. Two consequences matter to you as a buyer:
- Your delivery date carries real slack. A line that can pour your whole week’s order in a few hours absorbs a melt delay or a core hiccup without moving your ship date. Our casting lead time guide breaks down where the weeks actually go — and which ones automation compresses.
- The MOQ is negotiable arithmetic, not attitude. Fixed changeover and setup costs are what force minimum order quantities; a 30-minute changeover spreads that fixed cost over far fewer parts than a 4-hour floor setup. The mechanics are worked through in casting minimum order quantity.
There is a catch worth knowing: an automated line wants your part to fit its flask, its cope height and its pour node. Complex multi-core castings, very large parts and one-off fabrications still belong on the hand-finished floor — which is exactly why many suppliers run both and quote them differently. If your part needs a bespoke pattern strategy, the mold and pattern making capabilities behind the line decide as much as the line itself.
The ROI Math Behind Foundry Automation Investments
Understanding the payback your supplier runs explains their behavior — why they ask for your annual volume before quoting, and why some invest heavily while others stay manual. Three representative investments:
| Investment | Installed cost | Typical annual benefit | Payback | What it signals in your quote |
|---|---|---|---|---|
| Robotic finishing cell | $185,000 | $116,000 (labor + consumables) | ~1.6 years | Held piece price on 2,000+ parts/yr programs |
| Flaskless molding line | $1,900,000 | $410,000 (labor, floor space, scrap) | ~4.6 years | Needs steady 4,000+ molds/week — capacity for large programs |
| Robotic pouring cell | $420,000 | Modest direct savings; mostly quality | 5–8 years | Stable scrap on ductile iron; justified by escape risk, not wages |
Read the payback column and the volume question in your RFQ makes sense: a 1.6-year payback pays off on almost any serious program, while a 4.6-year payback only clears the hurdle if the shop can keep the line filled. Suppliers that quote automated prices without asking your annual volume either have the volume already — or are pricing optimistically.
How to structure the volume and price side of that conversation is covered in casting price adjustment clauses, and the tooling amortization rules that interact with line utilization are in casting tooling cost.
What to Ask a Supplier About Foundry Automation
Automation is a fact to verify, not a brochure line. When you prepare your casting RFQ, six questions separate real capability from decoration — the same discipline as the four numbers and scorecard in our casting supplier audit guide:
- Which operations are automated for my part specifically? Not the shop’s best cell — the cell your part runs on. A robot pouring automotive ductile iron does nothing for your hand-molded one-off base.
- What does the automated process control that a manual process would judge? Pour temperature band, mold hardness range, grind force — ask for the set points and the alarms.
- Show me the last three months of scrap data. A stable 2–3% is the signature of controlled pouring and molding; a 3–9% swing means the process, automated or not, is not in control.
- What happens when the cell is down? Every automated line has maintenance windows — a supplier running planned tooling maintenance on the line gives you honest lead times; one with no fallback lies to you about capacity.
- Where does my part cross between automated and manual operations? Most castings do. Machine-molded but hand-poured, or robot-poured but hand-finished — the seams are where inconsistency hides.
- How is my price indexed to that mix? If the finishing is robotic but the quote prices manual finishing, the margin belongs to you.
When Foundry Automation Does Not Matter
For programs under roughly 300 parts per year, very large castings, or parts with hand-set cores that take hours to place, the automation dividend shrinks to noise — a disciplined manual jobbing shop with tight 鋳鉄物 process control will outperform a poorly run automated line every time. Automation amplifies process discipline; it is not a substitute for it. The right question is never “how automated is this foundry” but “is the process that makes my part in statistical control” — whether that control comes from a robot or from a molder with twenty years of pattern experience and a written procedure. That judgment call — casting route versus CNC machining, or a hybrid approach — is covered from the cost side in CNC加工と鋳造の比較, and the surface-treatment steps that follow either route in casting secondary operations.
よくある質問
Does an automated foundry always produce better castings?
No. Foundry automation removes human-to-human variation, which makes a good process more repeatable — but it also repeats a bad setup at 150 molds per hour. Verify the process controls and scrap data, not the robot count.
Will foundry automation make my parts cheaper?
Usually it makes your price more stable first and cheaper second. The largest recoverable cost is finishing labor, so programs above roughly 2,000 parts per year see the clearest savings; below that, the fixed cost of changeovers dominates and manual jobbing shops remain competitive.
Can small buyers get parts from automated lines?
Yes, if their part fits the line’s flask and pattern envelope. Because an automated changeover costs a fraction of a manual setup, the volume that justifies a run is much lower — but very large, multi-core or one-off castings will still be routed to the manual floor or to prototype casting services.
How do I verify a supplier’s automation claims without an audit?
Ask for three artifacts that are hard to fake: the pour temperature log for a recent month, the scrap Pareto by defect type, and photographs of the actual cell with your part family on it. A shop with real foundry automation produces all three without hesitation; the rest produce explanations.
*Data referenced from AFS / NADCA / IFR industry publications and Supro MFG shop-floor records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina