
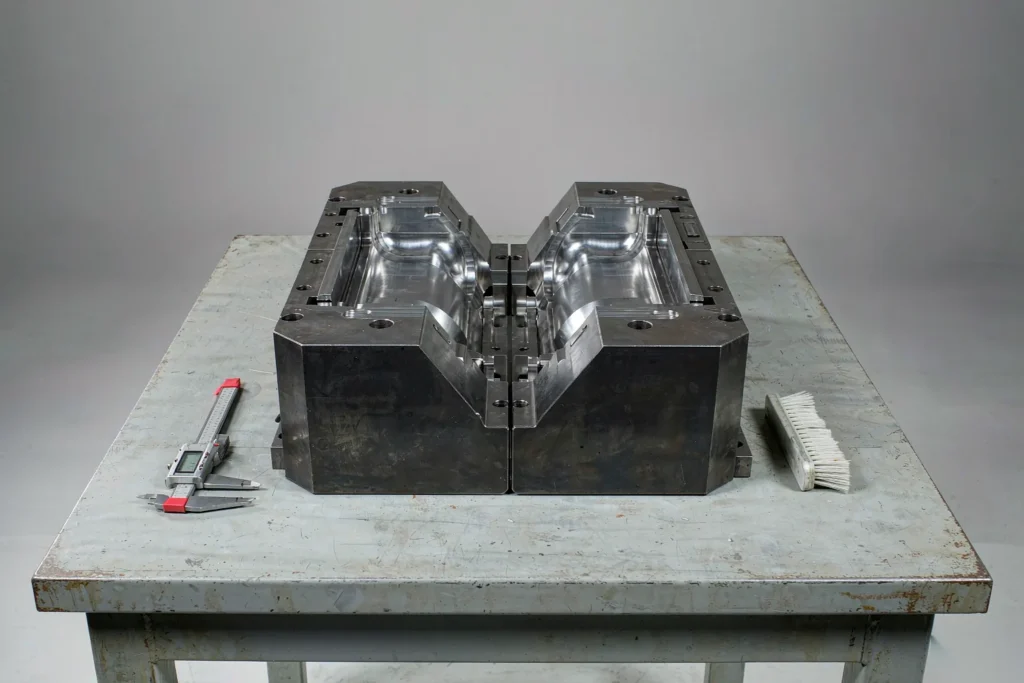
Tooling is the biggest one-time line on a casting quote, and it is also the largest hidden schedule risk in any repeat program. Buyers negotiate the price of the die and then never ask a second question. That is where the money leaks: disciplined casting tooling maintenance turns a 120,000-shot die into a 150,000-shot die and turns a five-day line stoppage into a two-day planned changeover. Skip it and the same asset quietly becomes your most expensive bottleneck.
This guide is written for the buyer and the engineer who pays for tooling but rarely sees the toolroom. If you need a refresher on the process families behind those numbers, start with our Guía de fundición de metales. It covers what casting tooling maintenance actually includes, realistic shot life by process, the six failure mechanisms and the check that catches each one, how to build a shot-based preventive maintenance schedule, the economics of refurbishment timing, spare cavity strategy, and the clauses worth putting in the purchase order. The numbers come from published ranges by the American Foundry Society (AFS) and the North American Die Casting Association (NADCA), with tool steel chemistry referenced to ASTM A681.
What Casting Tooling Maintenance Actually Covers
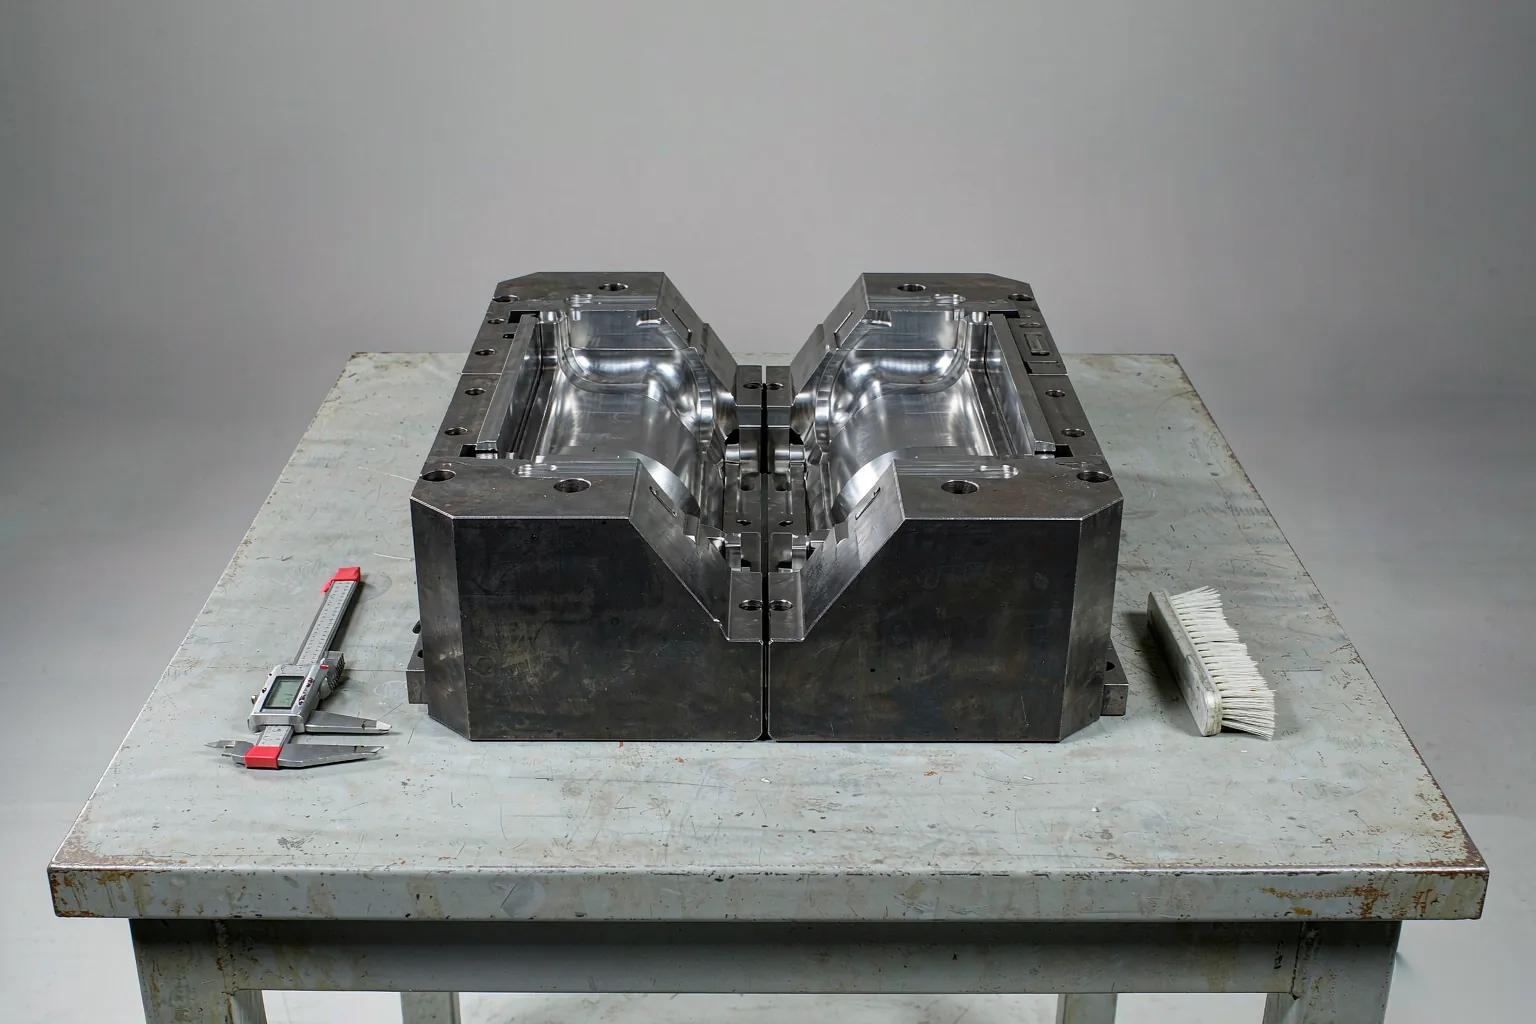
Most purchase orders say the foundry will “maintain the tooling” and stop there. That sentence covers three completely different activities with three different price tags. Separating them is the first step in making casting tooling maintenance a line item you can audit instead of a favour you hope for. Service access has to be designed in from the start, which is the argument we make in mould and pattern design. Disciplined casting tooling maintenance is not a workshop nicety; it is the difference between an asset that pays back and one that eats the program.
| Tier | Trigger | Typical duration | Typical direct cost |
|---|---|---|---|
| Production service | Every shift or every run | 15–40 min | Operator labour, already in the rate |
| Preventive maintenance (PM) | Shot or calendar counter | 4–8 h | $400–$900 per event |
| Refurbishment / rebuild | End of useful life, planned | 2–5 days | 18–30% of new tooling price |
| Emergency repair | In-run failure | 2–10 days, unplanned | Repair plus line-down cost |
The distinction that matters commercially is between the second and fourth rows. A scheduled PM is a predictable $400–$900 event folded into a planned changeover. An emergency repair on the same tool can easily cost $25,000–$35,000 once you add lost machine hours, scrapped work in progress and expedited freight to protect your customer’s line. The whole business case for casting tooling maintenance sits in that gap. It shows up again in any serious casting cost breakdown, where tooling amortisation is usually the second-largest non-material line.
Casting Tooling Maintenance Intervals by Process: Real Shot-Life Numbers
Tooling life is not a fixed number; it is a distribution with a long tail, and the width of that tail is mostly set by how the tool is serviced. The ranges below are the numbers used on shop floors when a program is quoted. If you are still choosing between routes for the same part, the volume crossover is set out in fundición a presión vs. fundición en arena. Treat the low end as “no meaningful maintenance” and the high end as “documented PM plus surface treatment”. Casting tooling maintenance is what moves you from the low end to the high end, and the spread is widest on routes like fundición en arena where pattern wear dominates.
| Proceso | Tooling material | Typical life | Dominant failure mode |
|---|---|---|---|
| High pressure die casting, aluminium | H13 (ASTM A681, 44–48 HRC) | 80,000–150,000 shots | Heat checking, then solder |
| High pressure die casting, zinc | H13, sometimes P20 for prototypes | 500,000–1,000,000+ shots | Gate erosion, flash build-up |
| Permanent mould, aluminium | H13 or alloyed cast iron | 30,000–100,000 cycles | Thermal fatigue cracking |
| Squeeze casting | H13, higher hardness 46–50 HRC | 25,000–80,000 cycles | Cracking at punch corners |
| Green sand, wood pattern | Hardwood or epoxy-faced | 500–2,000 moulds | Abrasion, moisture swelling |
| Green sand, metal pattern | Aluminium or cast iron | 25,000–100,000 moulds | Core print and locator wear |
| Shell mould / hot box | Cast iron, sometimes steel | 50,000–100,000 cycles | Sand erosion at the ingate |
| Investment casting wax die | Aluminium or tool steel | 10,000–50,000 injections | Parting line flash, slide wear |
| Lost foam foam tool | Aluminium, coated | 20,000–50,000 clusters | Bead vent clogging, coating wear |
Two things stand out. First, the same tooling steel gives you a 6× spread in life depending on how the tool is treated. Second, the process you pick sets the magnitude of tooling exposure before a single part is made — which is why tooling life belongs in the same conversation as casting tooling cost and amortisation, not after it. Our servicios de fundición a presión y fundición de aluminio teams quote tooling with a stated life range for exactly this reason.
Six Failure Mechanisms and the Check That Catches Each
Every tooling failure has a symptom on the part long before it has a symptom on the machine. Teaching your incoming inspection to read those symptoms is the cheapest form of casting tooling maintenance you can buy, because it converts a surprise into a scheduled event. The same early-warning logic drives the defect maps in our guide to defectos comunes en la fundición.
Heat checking and erosion
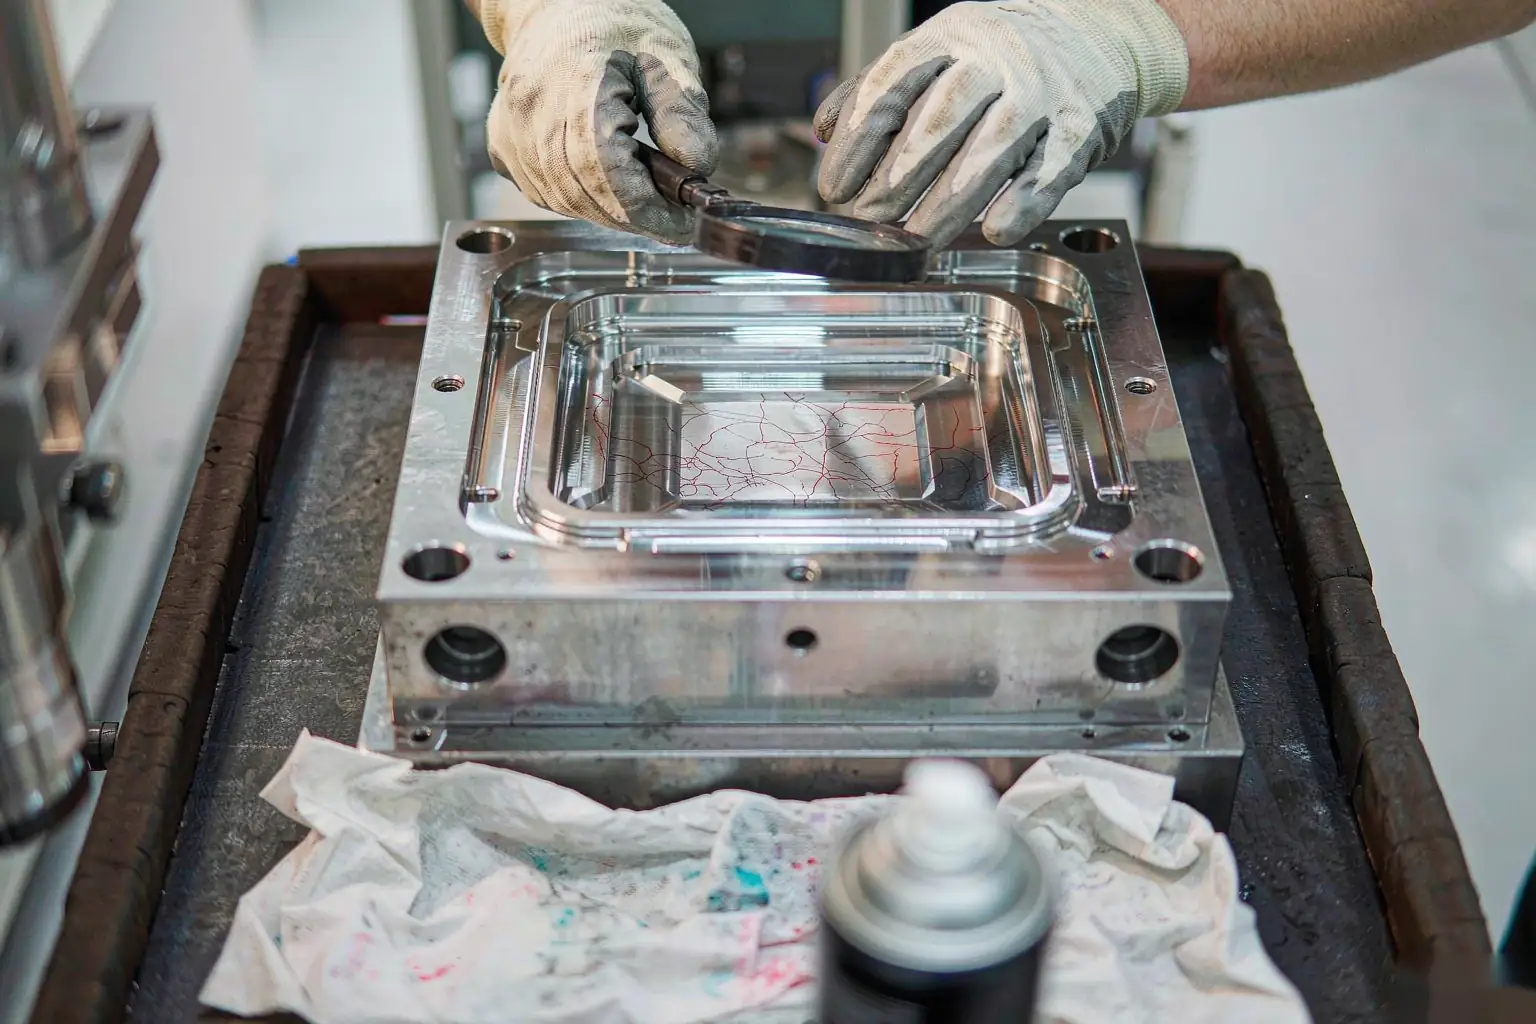
Thermal fatigue produces a network of fine surface cracks on the cavity face. On the part it shows up as raised veins or a frosted texture that grows shot by shot, and it is the standard end-of-life signal for fundición a presión de aluminio tooling. No amount of casting tooling maintenance reverses heat checking once it is deep; it only delays it. Erosion is different: it removes material rather than cracking it, usually at the gate and at any sharp change in flow direction, and on the part it shows up as a local thick band of flash or a drifting dimension on a wall that has always been stable.
| Mechanism | Symptom on the casting | Check | Interval |
|---|---|---|---|
| Thermal fatigue (heat checking) | Raised vein lines, frosted skin | Dye penetrant on cavity face | Every 25,000–30,000 shots |
| Erosion / washout | Growing flash band, drifting wall | Gate and ingate dimensional check | Every 10,000 shots |
| Soldering / galling | Torn skin on ejection, drag marks | Visual on cavity, ejection force log | Every shift |
| Corrosion in storage | Rust pits, first parts out of spec | Visual plus first-piece layout | Before restart after any idle period |
| Mechanical damage | Repeat burr in one fixed location | Parting face and shut-off inspection | Every tool pull |
| Dimensional drift | Slow trend on one feature, no defect | CMM or gauge R&R on critical features | Every 10,000–25,000 shots |
Dimensional drift is the dangerous one because nothing looks wrong. A core that has worn 0.05 mm does not create scrap; it moves the mean of a bore toward one limit and quietly eats your process capability. If you are already tracking capability on first articles, tie the tooling counter into the same review — the method is the same one used in first article inspection. The same counter belongs in your dimensional tolerance review, because tool wear and tolerance consumption draw on the same budget.
Build the PM Schedule Around Shots, Not the Calendar
Calendar-based servicing fails on tooling because a die does not age in weeks, it ages in thermal cycles. A tool that runs three shifts accumulates three times the damage of the same tool on one shift, and a calendar schedule treats them identically. The fix is a shot counter on the tool and a PM trigger written against that counter, with the calendar only as a fallback for idle periods. That single change is the backbone of effective casting tooling maintenance, and it also gives you a defensible number when a supplier quotes a replacement tooling lead time.
Worked example. A four-cavity aluminium die runs 8,000 shots per day across 22 production days per month, so it accumulates about 176,000 shots per month. Published life for that tool with no surface treatment is 120,000 shots. If the PM interval is set at 10,000 shots, that is 17 PM events per tool life — roughly one every three days of production, which is why the PM is folded into an existing changeover rather than booked as a standalone stoppage. Permanent mould casting y squeeze casting tools follow the same logic with wider intervals and lower shot counts.
The economics are easier than they look. One PM event costs about $500: four toolmaker hours at $95 plus around $120 in consumables and cleaning media. One unplanned failure on the same die costs:
- Line-down contribution. Five days at $2,400 per day of lost contribution = $12,000.
- Work in progress scrap. 1,800 pieces in process at $4.20 each = $7,560.
- Expedite freight. Air shipping 3,000 pieces to protect the customer line = $9,500.
That is $29,060 before anyone invoices a repair. So the break-even question is simple: a PM is worth doing whenever it cuts the probability of an in-run failure by more than $500 ÷ $29,060 = 1.7% over the interval. Once a die passes roughly 80% of its expected life, the interval failure hazard is well above that, which is why the interval should tighten rather than stay flat as the counter climbs.
Refurbishment Timing: A 35% Difference on the Same Die
Refurbishment means pulling the tool before it fails, stress-relieving or replacing the worn inserts, re-machining shut-offs, re-nitriding the cavity surface and re-certifying dimensions. Done once at the right moment it typically restores 60–80% of original life for 18–30% of new tooling price. Done a second time the return drops to roughly 30–50% of original life, and a third rebuild is usually money spent on a tool that should be replaced. Sequencing those decisions is the hardest part of casting tooling maintenance planning, and the tool steel condition behind them is covered in our tratamiento térmico de piezas fundidas guide.
Take a program of 360,000 shots over three years, running a four-cavity H13 die that costs $68,000 new with a 120,000-shot baseline life. Compare two policies.
| Line item | Reactive (run to failure) | Planned PM + one refurbish |
|---|---|---|
| New dies purchased | 3 × $68,000 = $204,000 | 2 × $68,000 = $136,000 |
| Refurbishment | $0 | $16,000 |
| PM events | $0 | 36 × $500 = $18,000 |
| Unplanned failure events | 2 × $29,060 = $58,120 | $0 |
| Total | $262,120 — $0.728 per shot | $170,000 — $0.472 per shot |
The planned policy saves $92,060 over three years, about 35%, and most of that saving is not the refurbishment — it is the two disasters that never happened. Long-running programmes in fundición de válvulas y automotive casting are where the gap between the two policies shows up most clearly. Note that the PM spend only pays because it extends life from 120,000 to 150,000 shots, letting two dies plus one rebuild cover the program instead of three dies. Good casting tooling maintenance is not a cost centre; it is a multiplier on the asset you already bought.
Surface treatments that change the numbers
Nitriding builds a 0.10–0.20 mm case at roughly 900–1,100 HV on the cavity surface and is the cheapest heat-check insurance available, typically +2–6% of tooling price for +30–60% life. Premium remelted H13 and higher-alloy die steels push further but carry a +15–25% tooling premium. Both are worth asking about at the quote stage, and both should be recorded on the tooling card so the next rebuild is specified from evidence rather than habit. Treated surfaces also change how a part releases and how the as-cast skin behaves in later surface finishing.
Spare Cavities and Inserts: Cheap Insurance
On a multi-cavity tool, the failure you should plan for is not the whole die — it is one cavity. A single damaged cavity insert costs roughly 8–12% of the full die price and can be built in 8–12 weeks against 16–20 weeks for a complete replacement tool.
Run the downside. On the four-cavity die above, one insert is about $6,800. If a cavity is lost with no spare on the shelf, output drops by 25% for ten weeks. At 2,000 pieces per day over 50 production days, that is 100,000 pieces of lost output; at $3.40 margin per piece the exposure is $340,000. Two spare inserts at $13,600 total against a $340,000 exposure is not a close call. This is also the argument for designing the tool with interchangeable inserts in the first place, which should be raised during tooling and mould making rather than after the die is cut. Many programmes validate cavity layout on a 3D printed prototype before the production tool is cut. Remember that tool wear also consumes machining allowance on the features that matter.
What Buyers Should Write Into the Tooling Clause
Tooling clauses usually cover price, ownership and nothing else. Five additional sentences turn a vague promise into something you can audit, and none of them should add cost on a well-run program. Casting tooling maintenance only works when the duty is unambiguous, and these clauses sit alongside the commercial terms you already negotiate, including minimum order quantities.
| Clause | Weak default | Better wording |
|---|---|---|
| Maintenance duty | “Supplier maintains tooling” | PM every 10,000 shots; full inspection every 30,000 shots |
| Shot counter | Not mentioned | Counter reading reported with each shipment |
| Life expectation | “Will last as long as needed” | Stated life range plus who pays below the floor |
| Refurbish notice | None | Notice at 75% of life, with quote and 15-day decision window |
| Idle storage | None | Rust preventive, sealed, slides exercised quarterly |
| Replacement lead time | “As required” | Committed weeks to a replacement tool, quoted up front |
The idle-storage clause matters more than buyers expect. A program that pauses for eight months comes back to tooling that has rusted, seized slides and a first-piece layout that no longer matches the last one. Requiring sealed storage with desiccant and a first-article re-check before restart costs almost nothing and removes an entire class of surprise. Put it in the same document as your acceptance criteria — the structure is identical to the one described in our guide to writing a casting RFQ. Where parts are finished in-house, the dimensional re-check belongs in the same pack as your Mecanizado CNC route sheet.
A Tooling Card You Can Actually Audit
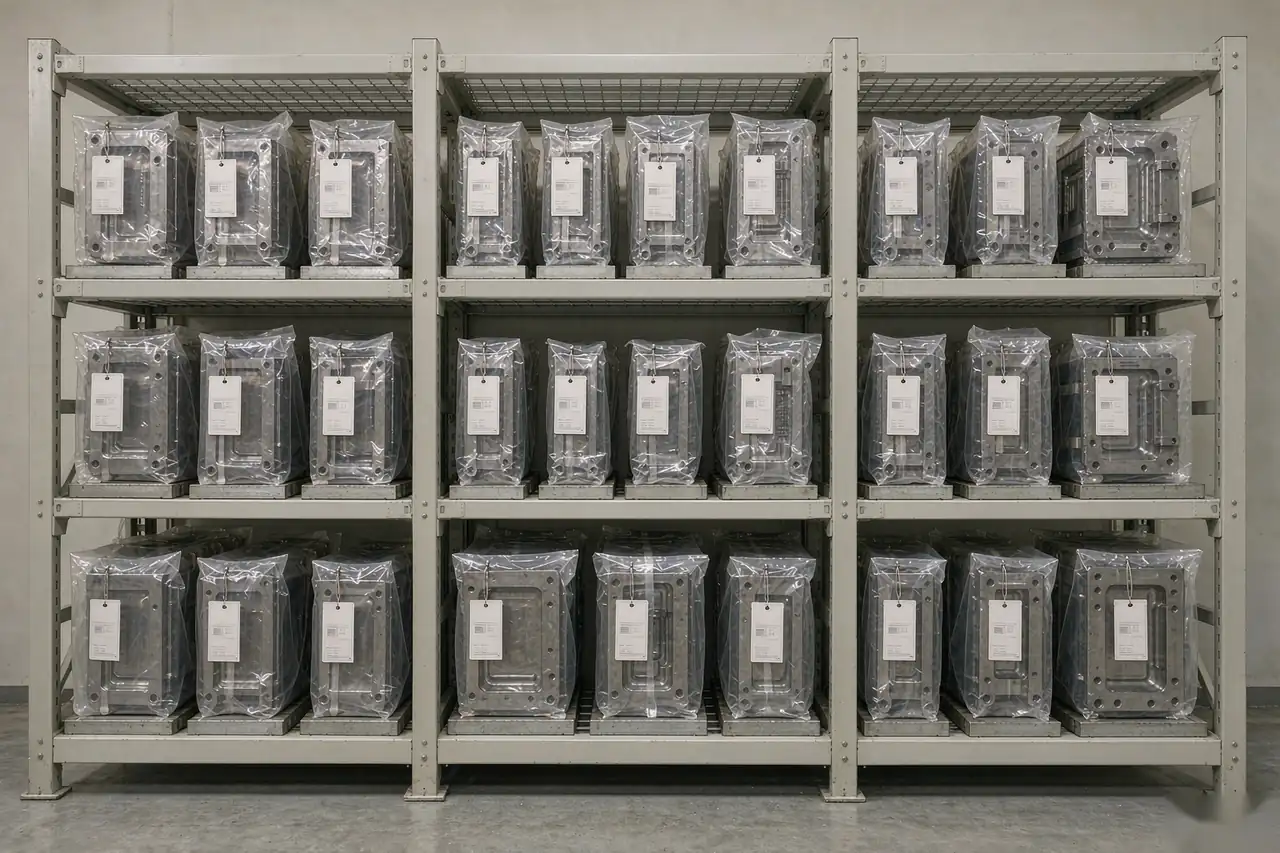
If a supplier cannot show you a record for a tool you own, the maintenance program does not exist, regardless of what the quote says. The record does not need to be software; a one-page card per tool is enough, and it should contain these eight fields. Without it, casting tooling maintenance is an assertion rather than a system.
- Tool identity. Part number, cavity count, build date, tool steel grade and hardness.
- Shot counter. Cumulative cycles and the date of the last reset after rebuild.
- PM history. Date, counter reading, findings, and what was replaced.
- Surface treatment. Nitriding or coating, with date and re-treatment trigger.
- Repairs. Welds, insert swaps, shut-off re-machining, with dimensions affected.
- Critical features. Which casting dimensions depend on which tool surfaces.
- Spares held. Inserts, ejector pins, cores on the shelf and their location.
- Next action. Counter reading at which the next PM or rebuild is due.
That last field is the one to ask for. A tooling card with a “next action” number means someone is planning; a card with only history means someone is reacting. It is the same discipline that separates a real capability study from a certificate folder, and it is worth the same weight when you inspect castings or audit the process behind them. On steel and iron programmes the card should also record grade and section thickness, because heavy sections raise cycle severity — the same reason fundición de hierro y cast steel grades are specified together.
Where the buyer owns the tooling outright, ask for the card to travel with the tool if production is ever moved. Tooling that leaves a plant without its history loses most of its remaining value, because the next shop has no baseline for the counter and no record of what has already been welded. Ask for the card at every program review: casting tooling maintenance reporting is the cheapest audit you will ever run. Shops that run solidification simulation on the gating system usually keep better records, because the two are reviewed together.
Preguntas frecuentes
How long does casting tooling actually last?
It depends on the process. Aluminium high pressure die casting tooling typically delivers 80,000–150,000 shots; zinc tooling runs 500,000 to over 1,000,000 shots; a metal sand casting pattern runs 25,000–100,000 moulds; an investment casting wax die runs 10,000–50,000 injections. Those ranges assume documented casting tooling maintenance, and the low end of each range is what you get without it. Shell tooling behaves differently again; see shell mould casting y lost foam casting for their own life windows.
Who pays for casting tooling maintenance during a program?
Routine casting tooling maintenance is normally absorbed into the piece price, because the supplier owns the process. Refurbishment and replacement are where it gets contested, and the answer should be written down: either the piece price carries a tooling amortisation component that funds the rebuild, or the buyer is invoiced separately with advanced notice. What you want to avoid is a price that funds neither, which is how a tool gets run past its life.
How often should a die casting die be serviced?
A practical schedule is a light service every 8,000–12,000 shots and a full pull-down inspection with dye penetrant every 25,000–30,000 shots, tightening the interval as the tool approaches 80% of expected life. The trigger should be the shot counter, not the calendar, and the work should be folded into an existing changeover wherever possible. Casting tooling maintenance schedules should always be written against the counter, never the calendar alone.
Can tooling be rebuilt more than once?
Usually once with good economics and twice only marginally. A first rebuild at the right moment restores roughly 60–80% of original life for 18–30% of new tooling cost; a second rebuild typically returns 30–50% of original life. By the third cycle, accumulated weld repairs and dimensional changes usually make a new tool the cheaper option. Wax tooling follows the same pattern with its own economics; see our fundición a la cera perdida capability for typical die construction.
What happens to tooling when a program goes idle?
It should be cleaned, coated with rust preventive, sealed with desiccant, and stored with slides and ejectors exercised periodically. If the tool ships with the programme, use the same export packaging discipline you apply to the parts. Sealed storage is the cheapest form of casting tooling maintenance there is. Before restart, expect a first-piece layout rather than assuming the last approved dimensions still hold. Tooling that sits unprotected for months is one of the most common sources of unexplained first-article failures.
How can a buyer tell whether maintenance is really happening?
Ask for the tooling card and look for two things: a cumulative shot counter and a next-action trigger. History without a forward trigger means reactive repair. If the supplier cannot produce a record for tooling you paid for, treat that as a finding about the whole quality system, not just about the toolroom.
*Data referenced from AFS / NADCA industry publications, ASTM A681 tool steel specification and Supro MFG shop-floor records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina