
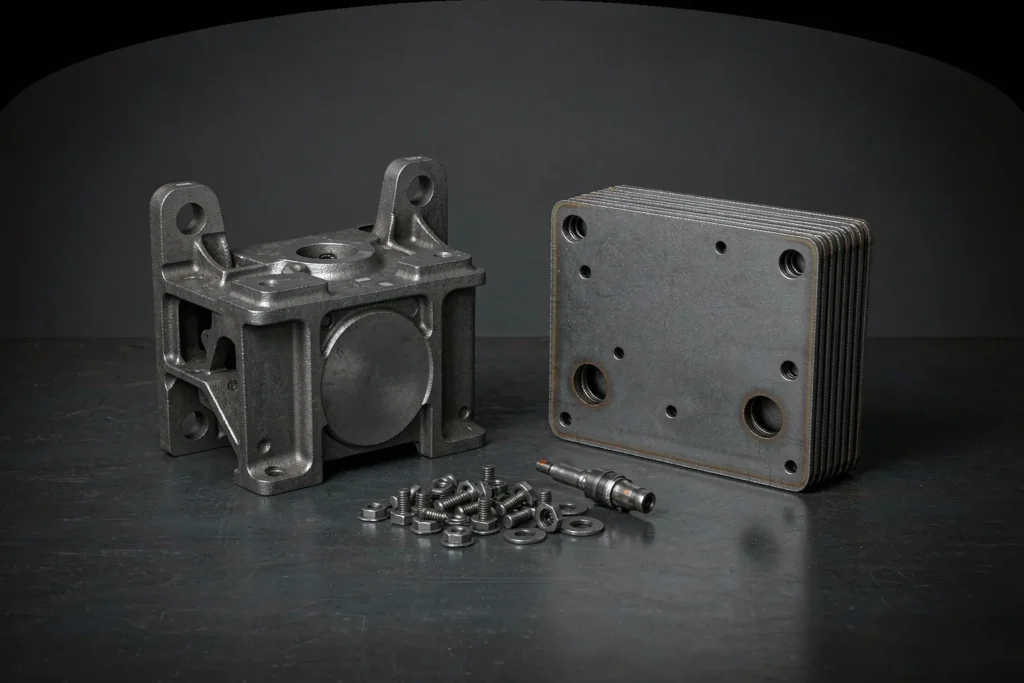
Casting part consolidation is sold as a design idea. On the shop floor it is a cost decision: you delete eight plate parts, ten bolts and five metres of weld, and you take on one pattern, one core box and one casting drawing. Whether that trade pays depends on a single number — how many units you build before the programme ends.
This guide gives you the arithmetic and the limits of casting part consolidation. Every figure below is a worked example built from real shop rates and standard solidification rules, not a rule of thumb. Where consolidation loses, we say so and show the number that kills it. For background on the process families referenced here, see the American Foundry Society, the North American Die Casting Association and the American Welding Society, and start with our own metal casting process overview if the process names are new to you.
What Casting Part Consolidation Actually Removes
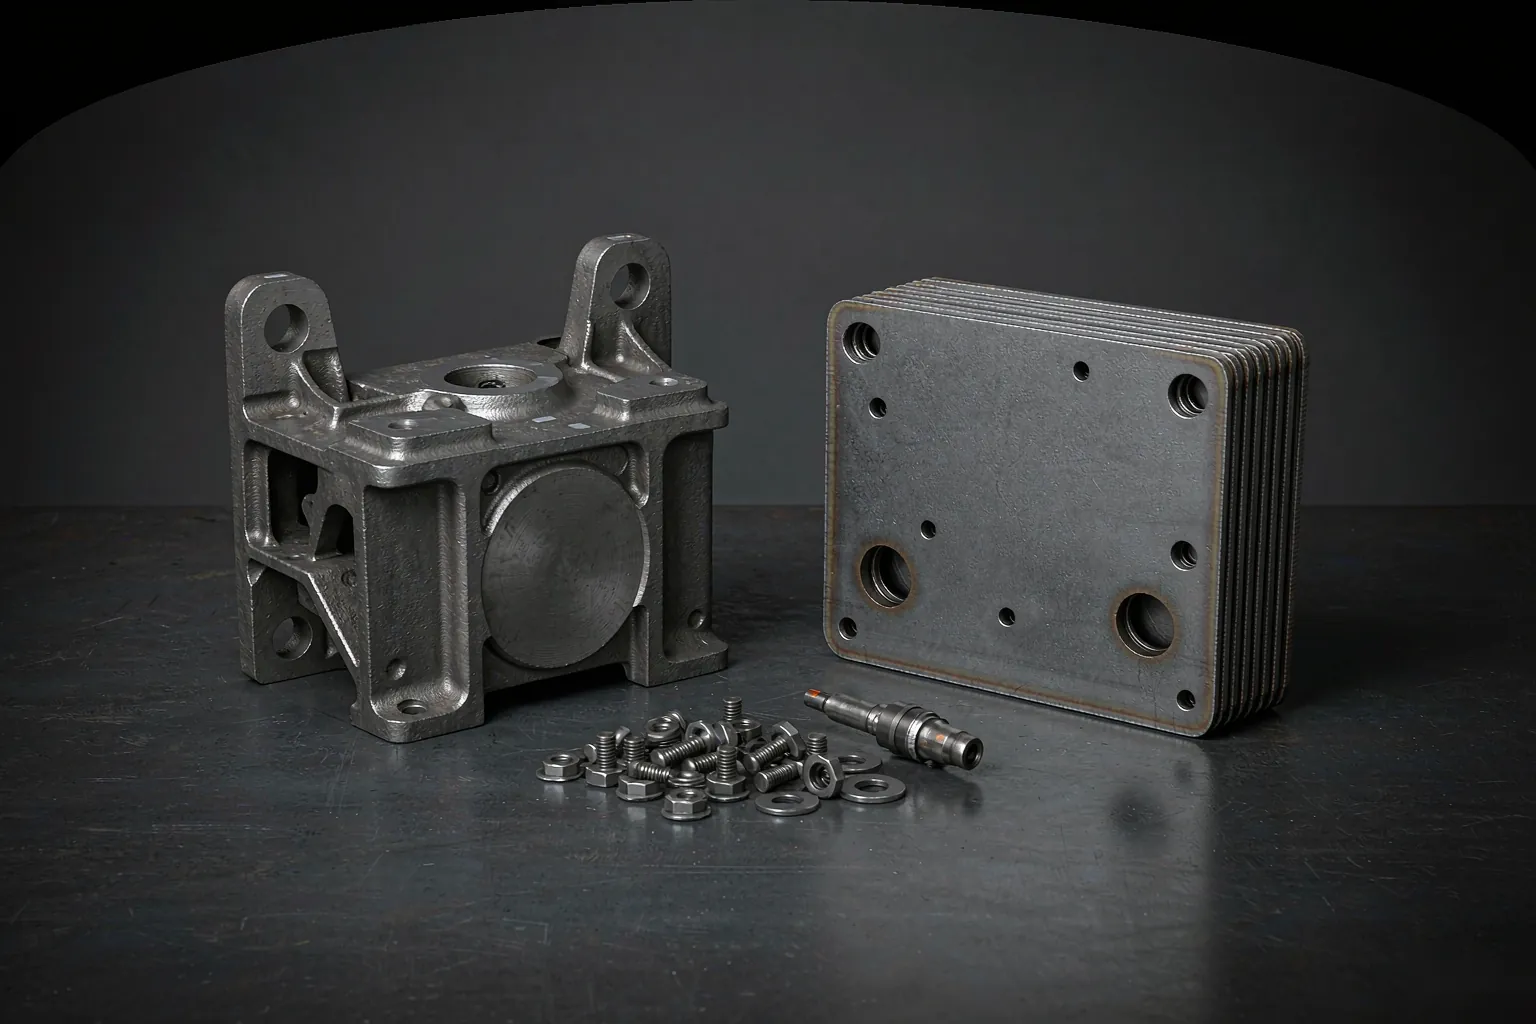
A welded or bolted assembly carries costs that have nothing to do with the shape of the part. Cutting, bending, fit-up, welding, grinding, stress relieving, fastener purchase, torque checks and final assembly all disappear at once when the assembly becomes one piece. At the same time, casting part consolidation takes on costs a weldment never had: tooling, a longer qualification loop, and a set of solidification risks that only exist once you put all the geometry into one body.
| Disappears | Appears |
|---|---|
| Cutting, bending and fit-up labour | Pattern and core box tooling |
| Weld metal, grinding and stress relief | Design, FEA and drawing release work |
| Fasteners, seals and torque records | Solidification risk at thick junctions |
| Multiple part numbers and their inventory | Longer first-article cycle before SOP |
| Leak paths and alignment stack-up | Minimum run quantity on every production batch |
Two of these lines decide most projects and they pull in opposite directions. Labour deletion saves money on every unit, forever. Tooling and engineering cost money once, before a single good part ships. That is why volume is the whole argument — and why our casting tooling cost breakdown should be read next to this one, alongside the wider picture in casting total cost of ownership.
Casting Part Consolidation Math: The Breakeven Number
The test for casting part consolidation is one line:
Breakeven units = (tooling + engineering + qualification + expected tooling changes) ÷ (weldment unit cost − casting unit cost)
If breakeven units is under roughly a third of your annual volume, consolidation pays back inside four months and the decision is easy. If it is more than about three times your annual volume, the payback stretches past three years and you are buying risk, not savings. Here is the full model for a real part.
Case A — 900 per year steel weldment
A machinery bracket built from eight laser-cut S355 plates, four bends, 5.6 m of 6 mm fillet weld, ten M12 fasteners, then machined on two setups. Shop rates used: welding and fitting at $72/h, machining at $95/h, inspection at $72/h. Deposition is taken at 2.0 kg/h with a 30% arc-on factor, which is why 0.79 kg of filler metal still costs 1.32 h.
| Cost line | Weldment | One casting |
|---|---|---|
| Material purchased | 27 kg plate × $1.35 = $36.45 | 14 kg casting × $2.95 = $41.30 |
| Laser cut + nesting | 18.4 m at 1.35 m/min + 0.30 h = $50.08 | — |
| Press brake, 4 bends | $38.00 | — |
| Fit-up and tack | 0.60 h = $43.20 | — |
| Welding | 0.79 kg filler, 1.32 h = $94.75 | — |
| Grind and blend | 0.70 h = $50.40 | — |
| Stress relief | 16 kg × $0.35 = $5.60 | — |
| Machining | 0.90 h = $85.50 | 0.35 h = $33.25 |
| Inspection | 0.30 h = $21.60 | 0.15 h = $10.80 |
| Fasteners | 10 × $1.85 = $18.50 | — |
| Final assembly | 0.40 h = $28.80 | — |
| Scrap and rework | +4% | +2% |
| Delivered unit cost | $491.80 | $87.06 |
Saving per unit: $404.74. Non-recurring cost: $6,400 pattern and core box, $5,800 design and FEA, $1,200 sample and first article inspection, plus an expected tooling change of 0.12 × $4,800 = $576 — $13,976 total. Breakeven is 34.5 units. At 900 per year that is under two weeks of production, and the first-year net is $364,266 − $13,976 − $609 of early-run scrap = $349,681. Purchased weight drops from 27 kg of plate to a 14 kg ductile iron casting.
Two things are worth noting before you copy these numbers. First, the weldment side is dominated by labour, not material — $412.33 of the $472.88 subtotal is labour and machine hours, which is why this comparison swings so hard towards casting. Second, the comparison is unfair to the weldment if your current assembly is already a cheap stamping design with spot welds instead of fillet welds; spot welding costs a fraction of arc welding per joint and closes most of the gap. If that is your baseline, read casting versus welded fabrication before deciding.
Where Casting Part Consolidation Stops Working
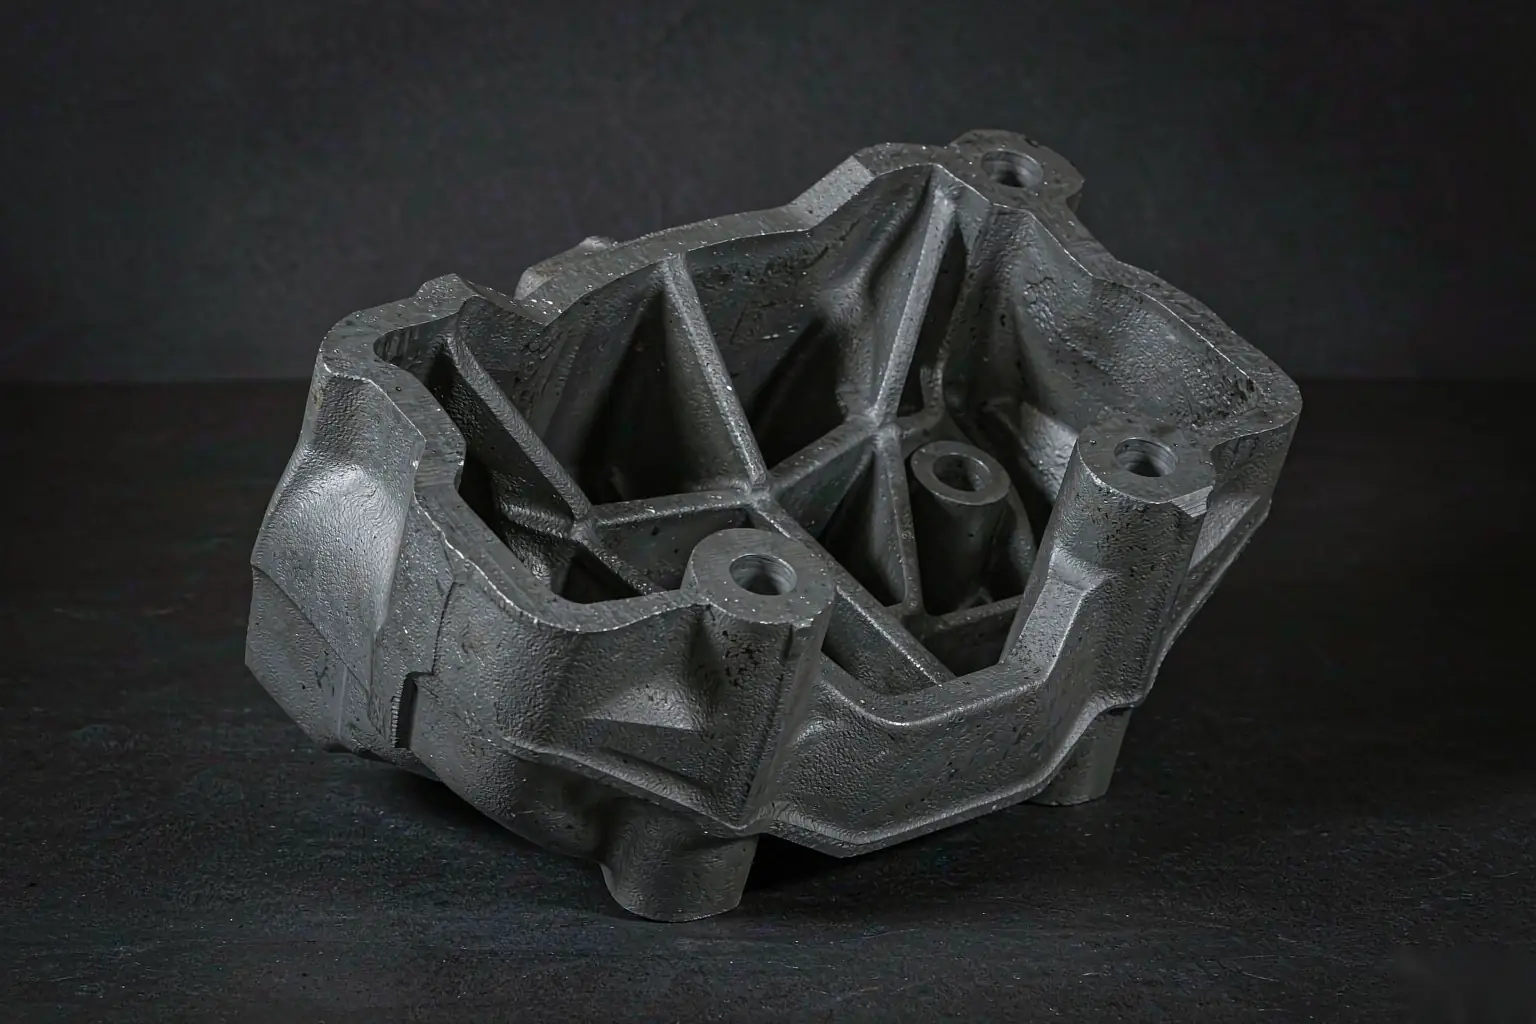
Case A is the easy one. The two failure modes that break casting part consolidation are volume that never recovers the tooling, and geometry that cannot be cast at all. Both are detectable before you spend a dollar.
Case B — 40 per year frame: the tooling never pays back
A 1.6 m frame currently welded from four plates: the weldment lands at $382.10 delivered. The consolidated casting weighs 26 kg and needs four cores, so it costs $76.70 + $24.80 of cores + $42.75 machining + $8.64 inspection, then a 5% allowance for casting scrap and core-shift rework = $160.53. Saving per unit is $221.57, which looks excellent until you put the tooling next to the volume: $18,400 tooling + $6,200 engineering + $1,400 qualification + $700 risk = $26,700, or 121 units to breakeven. At 40 per year that is three years, and the programme ends in three years. The honest answer is no — unless the same casting is shared with a sibling product at 55 per year, which pulls payback to 1.3 years and flips the decision. Sharing one consolidated casting across two products is the single most effective lever when volume is the blocker.
Case C — 400 per year aluminium: small parts, real tooling, still worth it
Two aluminium parts machined from plate plus eight fasteners: material $16.32, chip credit −$5.83, machining 0.84 h = $79.80, fasteners $8.80, assembly $25.20, inspection $14.40 → $142.85 with 3% scrap. One fundição à cera perdida at 0.62 kg × $12.80/kg plus 0.12 h of machining and a short inspection cycle lands at $24.13. Saving is $118.72 per unit; wax tool $4,900 plus fixture $3,000 plus $2,400 engineering = $10,300, so breakeven is 87 units. At 400 per year the first-year net is $37,187. Push the same part to 6,000 per year and a fundição sob alta pressão tool at $48,000 pays back in under 200 units instead — the process choice follows the volume, not the other way round.
| Case | Saving / unit | NRE | Breakeven | Volume | Verdict |
|---|---|---|---|---|---|
| A — steel weldment | $404.74 | $13,976 | 35 | 900/yr | Go |
| B — large frame | $221.57 | $26,700 | 121 | 40/yr | No, unless shared |
| C — aluminium pair | $118.72 | $10,300 | 87 | 400/yr | Go |
Prototype Before You Cut Production Tooling
Every casting part consolidation project carries one probability nobody writes down: the chance that the first tooling needs a correction. On our own work that sits around 12%, and a correction costs about $4,800 and four to six weeks. A printed sand mould set costs roughly $1,250–$2,400 and turns around in two to five days instead of four to six weeks for a pattern.
Run the expected value honestly. If a printed mould programme cuts the correction probability from 12% to 4%, it saves 0.08 × $4,800 = $384 of expected tooling. Against a $1,850 prototype that is a loss — on tooling risk alone the prototype does not pay. It pays on schedule, and schedule is the reason most casting part consolidation projects get a prototype at all. If the programme has a fixed SOP date and each week of slip is worth $9,000 in expediting, air freight or lost line time, then removing eight points of risk across a five-week correction is worth 0.08 × 5 × $9,000 = $3,600 of expected schedule exposure. That is the number that justifies the prototype, and it is a schedule argument, not a tooling argument.
There is a second benefit that is easy to miss: printed moulds and prototype castings can be poured in the production alloy, so the mechanical and dimensional data you collect is usable in the FAI package instead of being thrown away. See Protótipos impressos em 3D, metal prototype casting e mould and pattern making for the routes we run before cutting production tooling, and weigh them against 3D printing versus casting for volume parts.
Casting Rules That Break a Consolidated Design
Casting part consolidation concentrates geometry, and concentrated geometry creates thick junctions, long cores and walls that are too thin to fill. Four rules catch almost every problem before tooling is cut.
Minimum wall thickness by process
The wall you can cast is set by the process and the alloy, not by the load case. Use this table as the first filter on any consolidated design.
| Process and alloy | Practical minimum wall | Typical draft |
|---|---|---|
| Green sand, grey or ductile iron | 4–6 mm | 1–2° |
| Resin sand, carbon and low-alloy steel | 6–8 mm | 1.5–3° |
| Resin sand, aluminium | 4–5 mm | 1–2° |
| Shell mould, iron | 3–4 mm | 0.5–1° |
| Permanent mould, aluminium | 3.5–5 mm | 2–3° |
| High pressure die casting, aluminium | 2.0–3.0 mm | 1–2° |
| High pressure die casting, zinc | 1.0–1.5 mm | 0.5–1° |
| Investment casting, stainless steel | 2.0–3.0 mm | None needed |
Bosses, ribs and the modulus check
A solid boss is the classic shrinkage trap in a consolidated part. Take a Ø30 × 20 mm boss sitting on a 10 mm wall. Volume is 14,137 mm³ and the cooling surface is the side plus the top only, because the base merges into the wall — 2,592 mm². Chvorinov modulus is 5.45 mm against 5.00 mm for the wall itself (half the wall thickness). Solidification time scales with M², so the boss freezes 1.19 times later than the wall it sits on and will draw metal back out of it. On a machined face that shows as a 0.5–1.5 mm sink after facing. Core a Ø14 mm hole through the same boss and the modulus drops to 3.33 mm — now the boss freezes in 0.44 of the wall time and the wall feeds it instead. That is why the rule is boss OD at least 2× hole ID, and why our casting riser design guide treats feeding as the first check, not the last.
Rib thickness should sit at 0.6–0.8 of the wall, rib height below 5× rib thickness, and junction fillets at 0.5–1.0 of wall thickness. A consolidated design that keeps every wall within a 2:1 thickness range will almost always feed cleanly; one that jumps from 6 mm to 25 mm will not, no matter how good the solidification simulation looks. Shrinkage in these junctions is the single most common defect we see on first shots — see defeitos comuns de fundição for how it presents on the fracture face.
Cores have a length limit
Internal passages are what make casting part consolidation attractive, and they are also what kills it. A sand core supported at one end only behaves like a cantilever in liquid metal.
| Core length ÷ diameter | What it needs |
|---|---|
| Up to 3 | Single core print is enough |
| 3–5 | Longer print, or a second print opposite |
| 5–8 | Prints at both ends |
| 8–12 | Core supports or chaplets, with shift risk |
| Above 12 | Not castable in one piece — split it or drill it |
A 280 mm oil gallery on a 20 mm core is 14:1. It will not hold itself. Either the part becomes two castings with a bolted joint, or the gallery is drilled afterwards. Both are valid; neither is the saving you budgeted. Leave openings of at least 25 mm so core sand can actually be shaken out, and remember that every cored hole adds a machining allowance decision on the faces that get finished.
One part now means one alloy
An assembly lets each piece have its own material: a wear plate here, a machinable boss there, a cheap cover somewhere else. One casting has one chemistry and one heat treatment, and casting part consolidation quietly deletes that freedom. If a bracket needs a 55 HRC wearing face and 12% elongation in the arm, a single ductile iron grade cannot give you both. The honest options are a bolt-on wear plate, a localised heat treatment or a surface engineering route, or accepting a two-piece design. Check alloy capability early against seleção da liga de fundição, grey versus ductile iron, cast steel e aço inoxidável before the geometry is frozen.
A 20-Minute Screening Test Before You Redesign
Run these eight checks on the current assembly drawing before anyone opens CAD. Two or more failures means casting part consolidation is probably the wrong project for this part, and no amount of quoting will change that.
| Check | Pass condition |
|---|---|
| Volume | Annual units at least 3× breakeven units |
| Envelope | Fits the flask or machine with 80 mm of sand cover |
| Internal passages | Every core L/D at or below 12 |
| Single alloy | One grade covers every function on the part |
| Wall range | Thickest wall no more than 2× thinnest |
| Machining | All datums reachable in two setups or fewer |
| Shake-out | Openings of at least 25 mm for core removal |
| Programme life | Three or more years of production after SOP |
In practice, casting part consolidation pays best where the assembly is bolted and sealed: pump and valve bodies that used to be three pieces and two gaskets, automotive brackets built from five stampings, and agricultural frames where every bolt is a field-service failure point. It pays worst on sealed-for-life designs with a two-year model cycle.
How to Write the RFQ for a Consolidated Casting
Casting part consolidation produces a new part, not a revised one. Quote requests that treat it as a small change get vague prices back. Six things make the difference:
- Send the assembly as well as the casting model. The foundry needs to see what each feature used to do, which faces were sealed and which were structural.
- State the annual volume and the programme length. Tooling amortisation is the whole decision; without volume the quote is guesswork. See our casting RFQ checklist.
- Call out the tolerance grade per feature, not globally. ISO 8062-3 DCTG by feature is cheaper than one blanket grade — see tolerâncias de fundição.
- Name the acceptance standard for internal soundness. A radiographic class per ASTM E446 or a machining-based criterion, agreed before the first pour, as covered in casting inspection methods.
- Ask for the tooling breakdown separately. Pattern, core boxes, fixtures and expected life should each be line items, cross-checked against tooling maintenance expectations and the mould making route.
- Quote the finished part, not the raw casting. Machining and finishing are where the consolidation saving is won or lost — bundle secondary operations, Maquinação CNC e tratamento de superfície into one enquiry rather than three.
One more thing to budget on any casting part consolidation: the sample loop. Tooling, first shots, FAI and any tooling correction is a real schedule item that sits on top of normal casting lead time, and the finished part will ship through the same packaging and inspection gates as everything else. If you are running fundição em areia for the first time on this part, ask the foundry to walk the gating and feeding proposal with you before the pattern is cut — it is the cheapest hour you will spend on the project.
Perguntas frequentes
Does casting part consolidation always reduce weight?
Not always, but usually against purchased weight. Case A dropped from 27 kg of plate to a 14 kg casting. The saving comes from deleting lap plates, bolt flanges and weld overlap, not from thinner walls. If your assembly is already near net shape, weight will go up slightly, because a casting needs a minimum wall thickness and draft that a laser-cut plate does not.
How much tooling does a consolidated casting need?
Sand casting: one pattern plus one core box per distinct core, roughly $6,000–$20,000 depending on size and core count. Investment casting: a wax die plus machining fixtures, $5,000–$12,000 for small parts. Die casting: $30,000 and up for a multi-slide tool. Always ask for the breakdown by item and for the expected shot or mould life, then amortise it yourself — because casting part consolidation is decided by that amortisation, not by the casting price.
Can I consolidate a part that is already in production?
Yes, but treat it as a new part number with a new first article inspection. You will run two part numbers in parallel for a while, and you still owe spare parts for the old assembly. Build that carry-over cost into the business case — it is the line most often forgotten, and it is why consolidation is much easier on a new programme than on a running one.
Does casting part consolidation hurt dimensional accuracy?
Usually it improves it. An assembly accumulates the tolerance of every part plus fit-up error; one casting has a single tolerance chain. The trade-off is that a consolidated casting is bigger, and ISO 8062-3 tolerance grades widen with size, so a 1.6 m casting will not hold the same DCTG number in millimetres as a 300 mm one. Set per-feature tolerances rather than one global grade.
What is the smallest annual volume that justifies casting part consolidation?
There is no fixed number — it is breakeven units against programme life. A $13,976 NRE with a $404 saving per unit justifies 35 units, so even 100 per year is comfortable. A $26,700 NRE with a $221 saving needs 121 units, so 40 per year does not work. Compare the result with your real minimum order quantity e unit cost breakdown before committing.
*Cost models use $72/h weld and fit, $95/h machining, $72/h inspection; material at $1.35/kg plate, $2.95/kg ductile iron, $6.80/kg aluminium stock, $12.80/kg investment cast aluminium. Solidification figures follow Chvorinov (t ∝ M²). Data referenced from AFS / NADCA industry publications and Supro MFG shop-floor records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina