
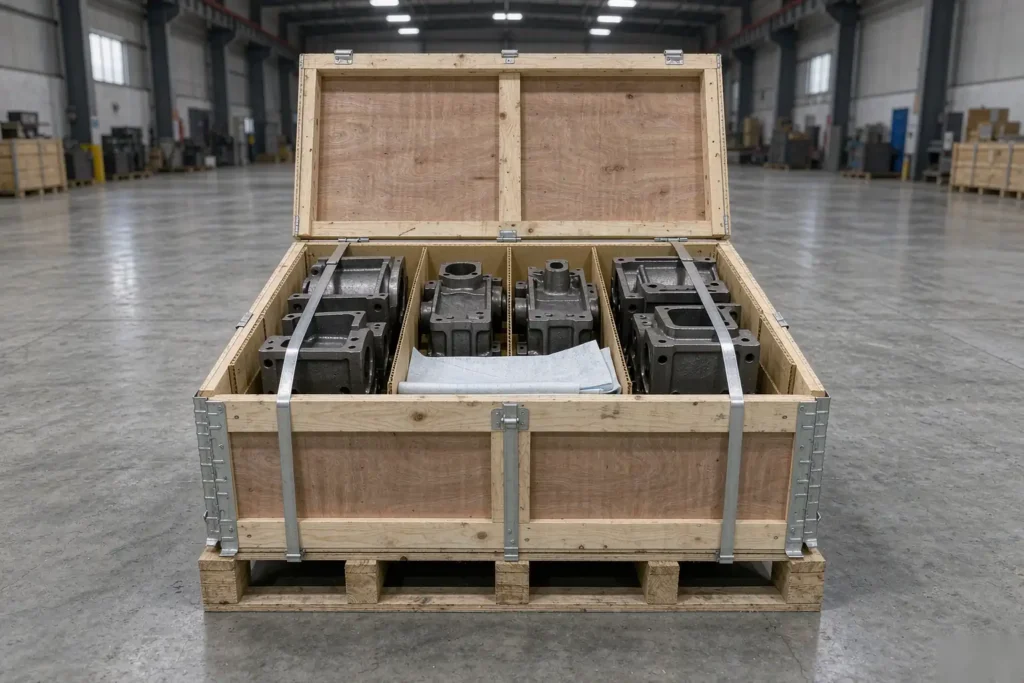
A container of castings can survive five weeks at sea and still fail the moment the crate is opened — rust blooms on a machined bore, a crushed bottom crate, a missing IPPC stamp that holds the shipment at customs. Casting packaging is the last process step nobody writes into the drawing, and the first one the buyer blames when parts land unusable.
This guide treats casting packaging as an engineering and cost problem, not a packing-list afterthought. It covers the four-layer protection system, how much water actually condenses inside a 40 ft container on a tropical route, what ISPM-15 means for your crates, how to size desiccant, and when an upgraded packaging spec pays for itself — with two cost models you can copy into your own RFQ. Standards and practice notes referenced from AFS 그리고 ASTM.
Why Casting Packaging Belongs in the Cost Model, Not the Packing List
Packaging typically runs 1.5–3% of landed part value for machined castings and 3–6% for heavy iron parts, because a crate heavy enough to survive stacking costs more than the corrosion protection inside it. That number looks small next to tooling or casting cost per piece, which is why it gets delegated to whoever is loading the truck.
The damage it prevents does not look small. A 1.8% arrival-defect rate on a 24,000-piece annual program is 432 parts that either get reworked, get scrapped, or trigger a customer complaint and an 8D report. Weighted at roughly $150 of real cost per incident part — rework labour, replacement value, freight both ways, and internal quality handling — that is about $65,000 a year decided by a $10-per-crate decision.
There is also a schedule dimension. Packaging failures are discovered at goods-in, weeks after the parts were made, so a replacement has to restart the whole chain — which is exactly the delay pattern mapped out in our casting lead time breakdown. A crate that costs $10 more is cheap insurance against a five-week loop.
If you are new to the process side, start with our 금속 주조 가이드 and then come back to this page — every casting packaging decision below depends on how the part was made, what alloy it is, and what condition its surface is in when it reaches the packing bench.
The Four Layers of a Casting Packaging System
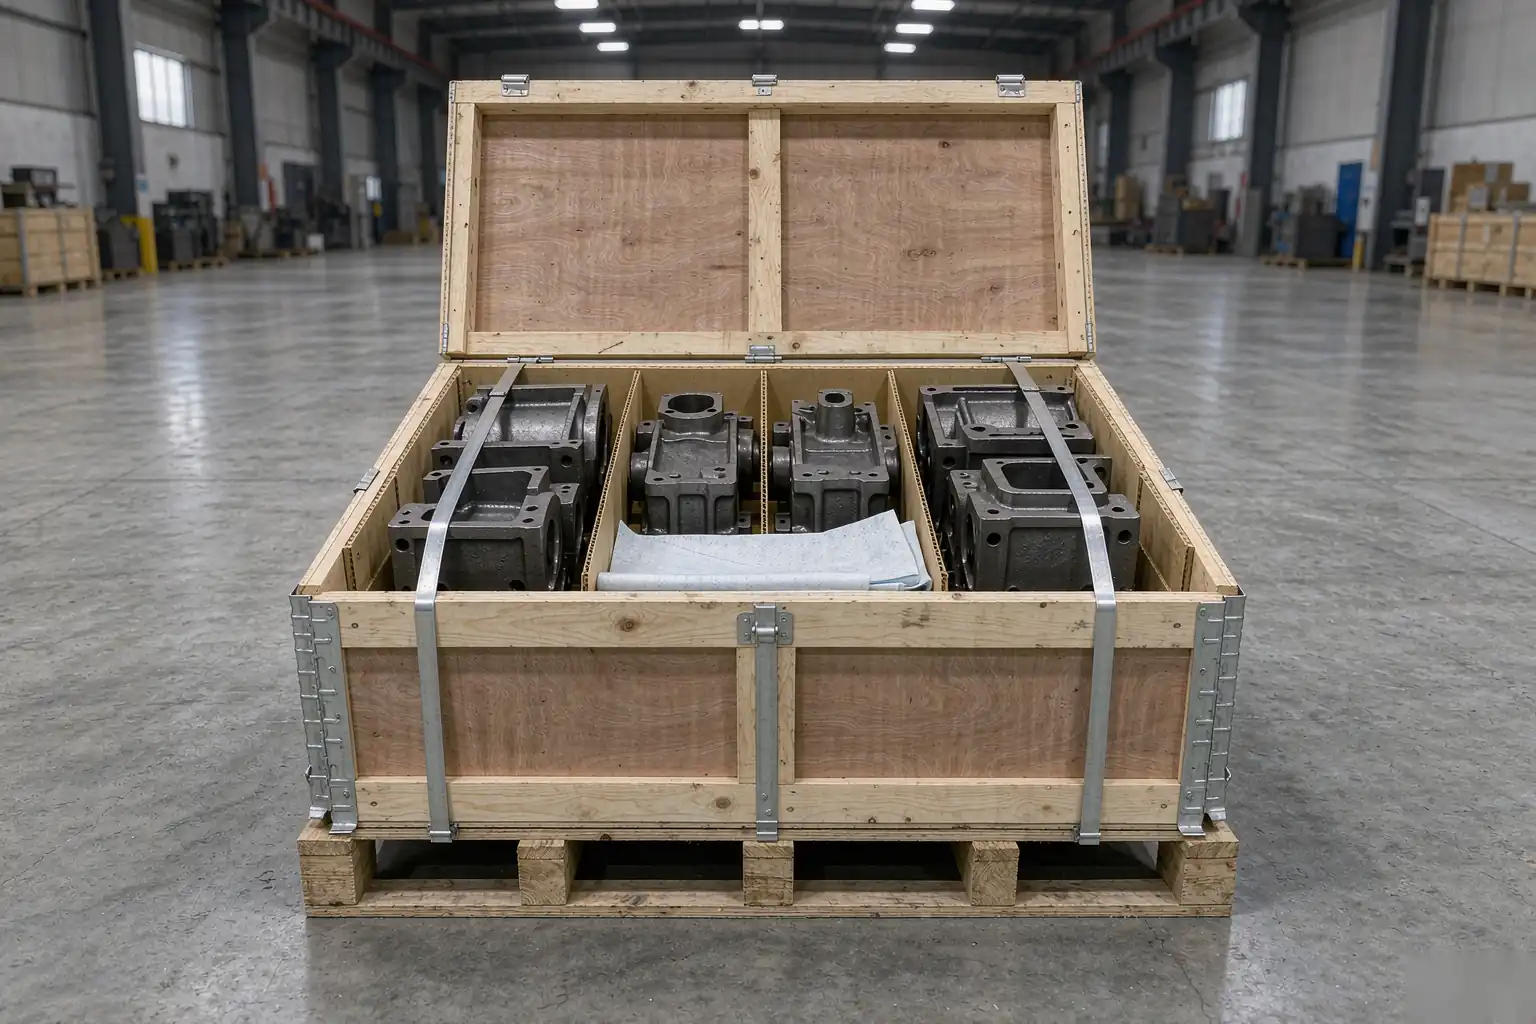
Every export-ready casting packaging build is four independent systems stacked on each other. Failures happen when one layer is asked to do another layer’s job — for example expecting a desiccant sachet to compensate for a crate that lets rain in.
| Layer | What it does | Typical materials |
|---|---|---|
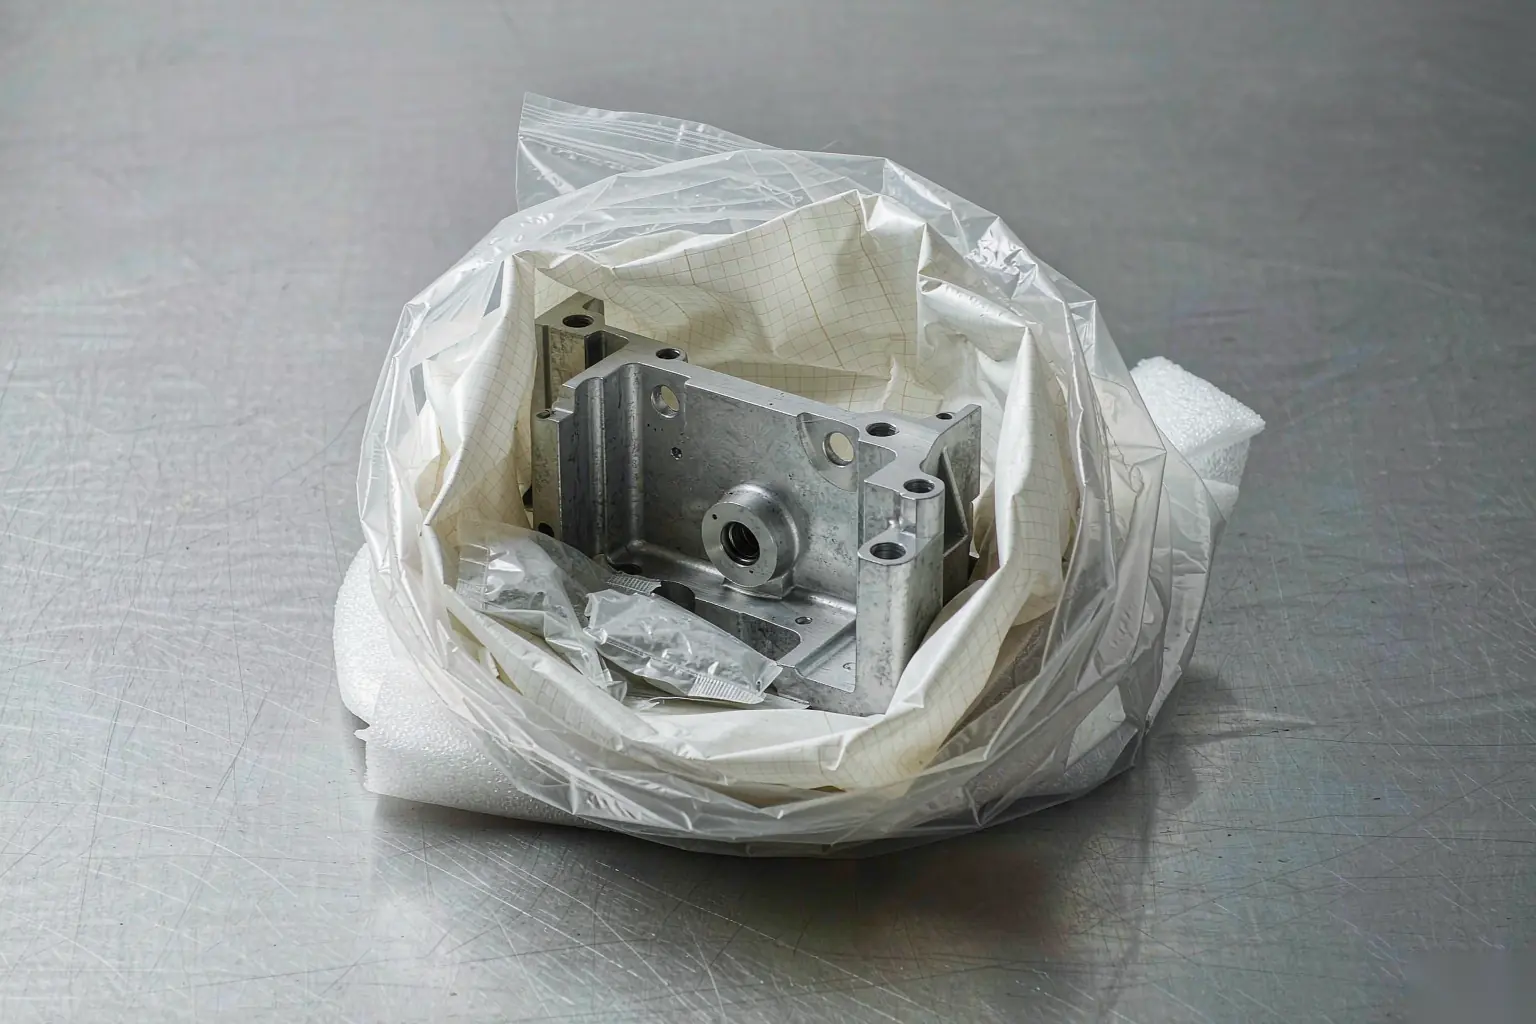
| 1. Surface protection | Stops corrosion on bare or machined metal | Rust-preventive oil, VCI paper or VCI film, primer or topcoat |
| 2. Moisture control | Keeps the micro-climate dry for the whole voyage | Desiccant (CaCl₂ or clay), PE liner, sealed bag |
| 3. Cushioning and separation | Stops part-to-part contact damage in transit | EPE foam sheet, corrugated dividers, edge protectors, dunnage |
| 4. Containment and unitisation | Carries stacking load, survives handling, moves as one unit | Plywood crate, pallet, steel or PET strapping, stretch film |
Layers 1 and 2 are chemistry; layers 3 and 4 are mechanics. Most buyer specifications get layer 4 right — everyone argues about crate thickness — and leave layers 1 and 2 to the supplier’s default, which is where corrosion claims come from. A good casting packaging spec states all four layers explicitly, because the supplier’s default is built for the cheapest route that usually works.
Layer 1 is not always a packing decision. If the part is primed, painted or otherwise treated before it reaches the packer, that treatment is the real first layer — see how 표면 처리 그리고 열처리 change what the packer is protecting. Writing a casting packaging clause without knowing the surface state is guesswork.
Rust Prevention: Oil, VCI, Desiccant or Coating
Pick the casting packaging protection method from the surface condition and the voyage length, not from habit. As-cast surfaces with intact mill scale or paint tolerate a lot; a machined bore at Ra 1.6 µm will flash-rust in a humid afternoon.
| Method | Typical salt-spray resistance (ASTM B117) | Best used for |
|---|---|---|
| No protection (as-cast, dry store) | 4–8 h before first rust spots | Domestic or short inland moves only |
| Thin rust-preventive oil film | 24–72 h | Machined faces on short sea legs; cheap, but needs degreasing at goods-in |
| VCI paper or VCI bag, sealed | 200–400 h equivalent protection in a closed pack | Default for machined castings on 30–45 day ocean routes |
| Primer or topcoat (epoxy, polyurethane) | 500–1,000 h | As-cast parts stored outdoors at destination; see casting surface finishing |
| VCI + desiccant + PE liner (combined) | Voyage-rated, not hour-rated | High-value machined parts, tropical routes, long dwell at port |
How much water actually condenses inside a 40 ft container
“Container rain” is not a myth, and it is easy to size. Take a 40 ft high-cube container with 76 m³ of internal volume loaded on a humid day:
- Air at 30 °C / 80% RH holds about 24.3 g of water per m³ → 76 × 24.3 ≈ 1.85 kg of water vapour in the box.
- Cooled overnight to 15 °C, saturation drops to about 12.8 g/m³ → only 0.97 kg can stay airborne.
- Difference ≈ 0.88 kg condenses on the coldest surface available — usually the container roof, then drips onto your crates.
The bigger source is the wood itself. A crate and pallet set weighing 250 kg at 15% moisture content carries about 37 kg of water; a 35-day voyage releases a few percent of that into the box — roughly 1.5 kg in our example — and the day/night condensation cycle repeats every night of the trip.
So the first-cycle load is about 2.7 kg (0.9 kg from air + 1.5 kg from wood + ~0.3 kg from cartons and dunnage), and it recurs. That is why the practical industry rule for a 40 ft box is 12–16 kg of desiccant (roughly 24–32 sachets of 500 g CaCl₂), not the 3 kg the single-cycle arithmetic suggests. Specify the desiccant type and count in the packaging clause — “include desiccant” is not a specification.
Sizing desiccant for the air and forgetting the wood is the most common casting packaging mistake we see on inbound claims: the sachets are present, the count was never calculated, and the parts still arrive wet. Aluminium parts are especially unforgiving here — see white rust and corrosion on aluminium castings for what humidity does to bare alloy surfaces.
Crates, Pallets and ISPM-15: The Compliance Layer
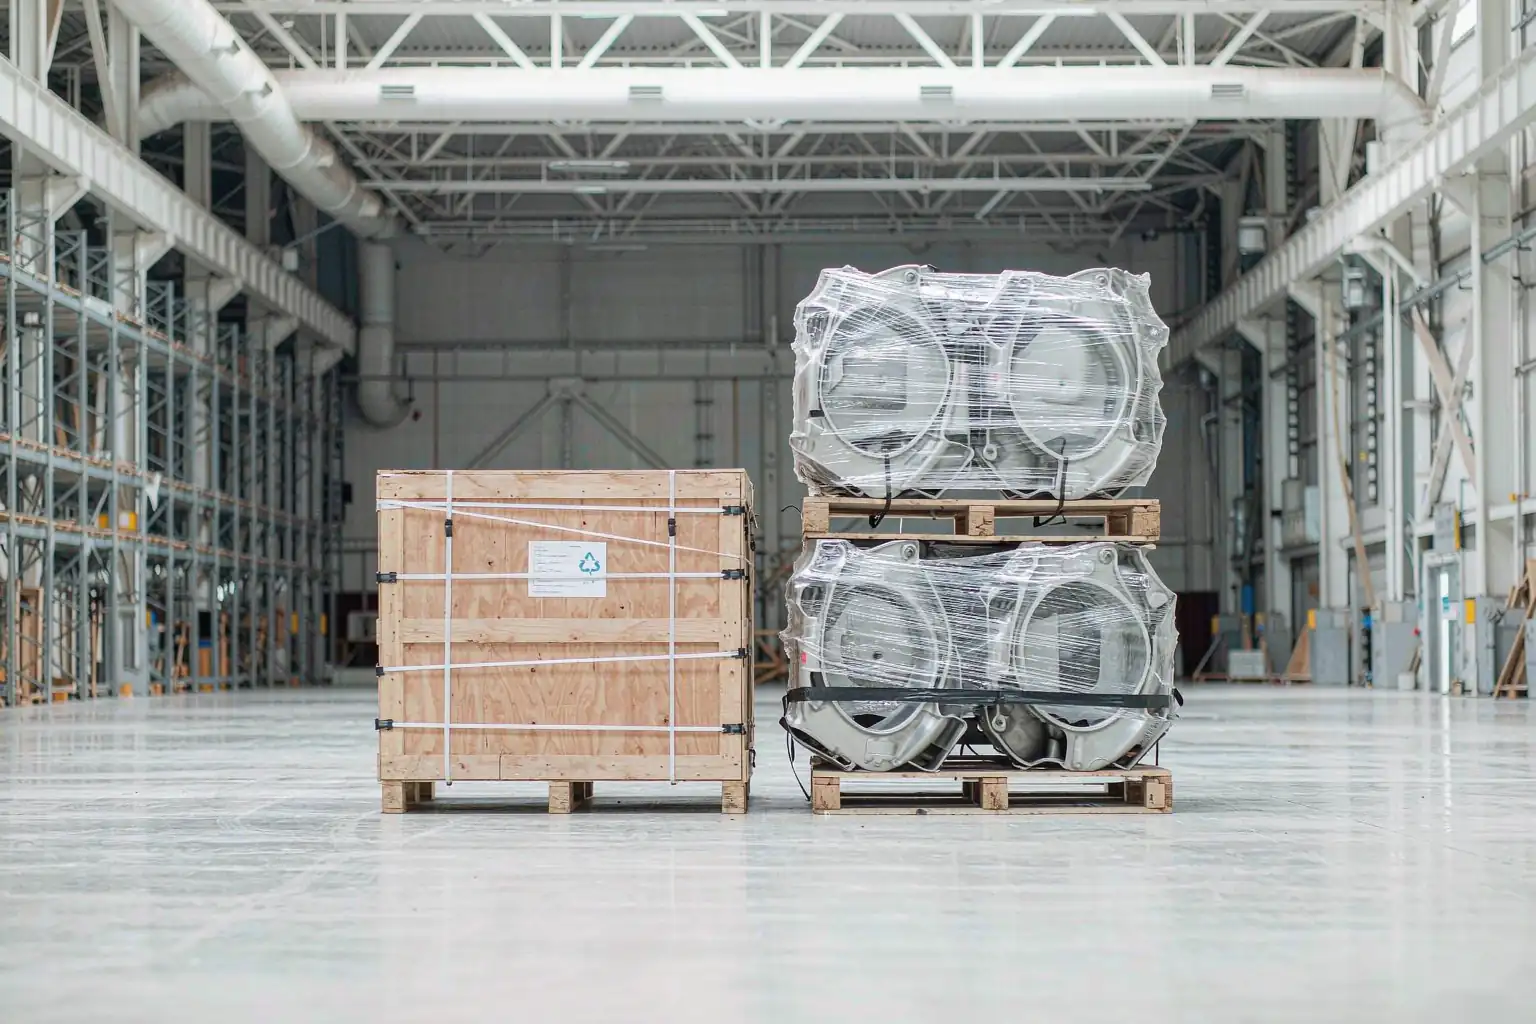
Solid wood packaging moving across most borders must be treated and marked under ISPM-15: heat treatment to a minimum core temperature of 56 °C for 30 minutes, or fumigation, then stamped with the IPPC symbol, country code, treatment provider number and the treatment code (HT or MB). Plywood, OSB and other engineered wood panels are already exempt — they are manufactured under heat and pressure — which is why plywood crates remove the compliance risk entirely.
The casting packaging failure mode here is expensive and dumb: an unmarked or wrongly marked crate can be held at destination for re-treatment, fumigation, or re-export, at four-figure cost per container plus weeks of delay. If your route includes the EU, US, Australia or China, put “ISPM-15 compliant, HT-marked, or engineered panel crate” in writing.
Stacking load: design the bottom crate, not the top one
Crates are usually stacked three high in a container and sometimes four in a warehouse. A 480 kg crate in a three-high stack means the bottom crate’s lid and side panels are carrying 960 kg of static load — before any dynamic factor from road or rail vibration. That is the number to give your supplier: “crate must carry 2× its own gross weight in a three-high stack.”
Practical details that decide whether that holds: continuous bottom runners (100 × 100 mm is a common minimum for heavy iron), panels screwed rather than nailed at the corners, strapping over the lid and around the base, and a pallet base that lets a forklift enter from at least two sides. Corner protectors under the strapping stop the strap from crushing the panel edge — a common cause of lid damage on arrival.
Container loading: know whether you are volume-limited or weight-limited
A 40 ft high-cube box gives you roughly 65 m³ of usable volume and a payload of about 22,800 kg net (26,500 kg gross limit minus ~3,700 kg tare). Which limit bites first depends entirely on the alloy:
- Aluminium housings, 6.5 kg each. 32 parts per 1,200 × 800 mm pallet at 1.1 m height = 1.056 m³ and 233 kg per pallet. Volume limit: 65 ÷ 1.056 ≈ 61 pallets ≈ 1,950 parts, weighing only 14,200 kg — volume-limited, with payload to spare. Typical of high-volume 다이캐스팅 그리고 aluminium casting programs.
- Ductile iron valve bodies, 42 kg each. Six per crate at 0.297 m³ and 274 kg gross. Weight limit: 22,800 ÷ 274 ≈ 83 crates ≈ 498 parts, filling only 24.6 m³ — weight-limited, using 38% of the volume. Typical of 모래 주조 그리고 밸브 주조 work.
That second case has a trap: the ISO payload is not always the binding limit. Many inland trucking legs, particularly in North America, cap 40 ft cargo closer to 19,000–20,000 kg, which cuts the iron example to about 70 crates. Always confirm the routing weight limit before you quote a container quantity for heavy castings — and if your parts are iron or steel, check the 주물 그리고 강철 주조 pages for typical piece weights before you plan a load.
Machined Surfaces Need a Different Casting Packaging Spec
A single crate of casting packaging often contains both as-cast and machined surfaces, and they do not need — or tolerate — the same treatment. Machined faces must arrive clean and dry, so heavy greasing creates a degreasing step at goods-in; as-cast faces are rough enough to hold a coating and are far less corrosion-sensitive when painted.
| Surface condition | Minimum protection for ocean freight | Separation requirement |
|---|---|---|
| As-cast, blasted, unpainted | VCI + desiccant; no oil needed if packed dry | Cardboard or foam between parts |
| As-cast, primed or topcoated | Paint film intact; touch-up before packing | Edge protectors at contact points |
| Machined, Ra 1.6–3.2 µm | VCI paper wrap or bag + desiccant + sealed PE liner | Individual wrap, no part-to-part metal contact |
| Machined + threaded holes or bores | VCI plus plugs or caps on threaded features | Plastic caps; foam sheet between layers |
| Machined, customer-specified clean (no oil) | VCI only — oil is prohibited by spec | Sealed bag with desiccant inside the bag |
Where machined faces come from a CNC route rather than the foundry, agree the packaging interface in writing: the foundry ships protected as-cast parts, the machining shop re-protects after cutting. Our CNC 가공 서비스 그리고 casting machining allowance guide both assume the final packer owns that last protection step.
Near-net-shape processes change the requirement again. 정밀 주조 parts often arrive with tight as-cast tolerances and cosmetic surfaces that must not be marked by contact, while lost wax casting parts with fine detail need individual cushioning rather than bulk dunnage. In both cases the casting packaging spec has to be written per part family, not per shipment.
Labels, Lot Numbers and the Packing List
Casting packaging is also the last chance to carry traceability into the customer’s warehouse. Every crate should be labelled with part number, revision, purchase order, heat or lot number, net and gross weight, and crate sequence (1 of 24). The lot number on the crate must match the lot number on the inspection report — that link is what makes an first article inspection package usable at goods-in six weeks later.
- Shipping marks. Stencil or printed label on at least two adjacent faces of each crate; ink that survives condensation, not a paper label under the strapping.
- Barcode. GS1-128 or Code 128 on the crate label, encoding part number and lot — scanning beats transcription when 24 crates arrive at once.
- Packing list. One line per crate, weights and counts matching the marks, plus a waterproof copy taped inside crate #1 and an emailed PDF set sent on departure.
- Handling marks. “This way up”, sling points, and centre-of-gravity marks on anything over 500 kg — a crate that tips in the yard is a crate that arrives damaged.
For programs that already specify incoming inspection, align the crate count with the sampling plan so a lot is not split across crates in a way that forces opening everything. The sampling maths in our 주조 검사 방법 article assumes lots are identifiable as packed.
What to Put in the Packaging Clause of Your Casting RFQ
Casting packaging is one of the fastest ways to make a quote comparable between suppliers, because it is invisible until it fails. Add these lines to the RFQ — the rest of the request is covered in our casting RFQ checklist:
- Voyage profile. Destination port, expected transit days, and whether there is outdoor storage at destination. 35 days through the tropics and 12 days to Rotterdam are different specifications.
- Surface protection. VCI type and grade, or oil type if oil is allowed, and whether machined faces must arrive oil-free.
- Desiccant. Type and total mass per crate, plus per-container total. Write the number, not “as required”.
- Crate spec. Plywood or ISPM-15 HT solid wood, panel thickness, runner size, strapping, and the stacking load the crate must survive.
- Parts per crate and crate dimensions. Fixes the container count and the freight quote, and stops the “we optimised it later” surprise.
- Labelling and documents. Mark content, barcode format, packing list format, and whether photos of the loaded crate are required before release.
Ask for photos of the first crate — closed, strapped, and labelled — before the container is sealed. It takes a day and prevents an entire shipment going out with the wrong marks.
When an Upgraded Casting Packaging Spec Pays for Itself
Two annual programs, one upgrade decision each. Both use the same incremental package: VCI wrap, two extra 500 g desiccant sachets, and EPE dividers plus edge protectors — about +$10.30 per crate. No change to crate type, which is the point: the expensive part of casting packaging is the crate, and you rarely need to change it.
| Item | Case A — machined aluminium housing | Case B — painted ductile iron pump body |
|---|---|---|
| Annual volume / parts per crate | 24,000 / 12 → 2,000 crates | 8,000 / 6 → 1,333 crates |
| Voyage | 35 days, tropical route, machined faces | 12 days, temperate route, painted as-cast |
| Arrival defect rate today | 1.80% → 432 parts/year | 0.40% → 32 parts/year |
| Annual damage cost today | $53,424 (rework $10,944 + scrap $37,440 + 12 complaints $5,040) | $3,840 (~$120/part weighted) |
| Rate after upgrade | 0.45% → 108 parts/year | 0.25% → 20 parts/year |
| Annual damage cost after | $13,356 | $2,400 |
| Upgrade cost | 2,000 × $10.30 = $20,600 | 1,333 × $10.30 = $13,730 |
| Net annual result | +$19,468 saved (ROI ≈ 1.9×) | –$12,290 — do not upgrade |
The rule that falls out of the two cases: an upgraded casting packaging spec pays when the voyage is long and the surfaces are machined. Break-even in Case A is a defect-rate reduction of about 0.57 percentage points (137 parts/year × ~$150 weighted cost ≈ $20,600); the measured reduction is 1.35 points, so there is real margin. In Case B the whole annual damage bill is smaller than the upgrade cost, so the money belongs in crate strength and paint integrity, not in VCI and desiccant.
One more casting packaging lever that costs nothing: reduce the number of crate openings at destination. If parts are packed in the sequence the line consumes them, they spend less time open in a humid warehouse — which is where a surprising share of “arrival rust” actually happens.
자주 묻는 질문
How much does export casting packaging add to part cost?
Typically 1.5–3% of part value for machined castings and 3–6% for heavy iron parts, where the crate itself dominates. Casting packaging is quoted per crate, so the honest way to compare two suppliers is cost per shipped part, not cost per crate. On a $180 machined housing that is roughly $3–5 per part; on a 28 kg iron body it is closer to $3–6, mostly crate and pallet.
Is VCI enough, or do I also need desiccant?
For a 30–45 day ocean voyage, use both. VCI protects the metal surface chemically; desiccant removes the water that would otherwise condense and drip. Our 40 ft example generates about 0.9 kg of condensation from the air alone on the first night and roughly 1.5 kg from the wood over the voyage, which is why the practical desiccant load is 12–16 kg per 40 ft container.
Do plywood crates really avoid ISPM-15 treatment?
Yes. Plywood, OSB, particleboard and similar engineered panels are manufactured under heat and pressure and are exempt from ISPM-15 treatment and marking. Solid wood — including pallets, dunnage and bracing — is not exempt and must be HT- or MB-treated and stamped.
Who is responsible for packaging under FOB versus EXW?
Under FOB the seller packs for export and loads the vessel; under EXW the buyer collects, so the buyer must specify the export packaging in the order or the parts will arrive in domestic packing. Either way, write the packaging clause into the PO — the Incoterm allocates cost, not the specification.
Can we send our own casting packaging specification?
Yes, and you should if you have one — a written crate, VCI and desiccant spec removes the biggest variable between quotes. Send it with the drawing and the RFQ through the contact page; if you do not have one, ask the supplier to state the four layers in their quote so you can compare like for like.
Can packaging hide defects that inspection should catch?
It can delay their discovery, which is worse. Rust found at goods-in six weeks after shipment makes root-cause analysis almost impossible — you cannot tell whether it came from the foundry, the packing bench, or the container. Photograph parts at packing, keep a retained sample, and inspect on arrival against the same tolerance and condition criteria used at source.
*Data referenced from AFS / ASTM / IPPC (ISPM-15) publications and Supro MFG shipping records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina