

In B2B precision manufacturing, the decision between cnc machining vs casting is rarely black and white. Both processes deliver metal parts—but at different cost structures, tolerance windows, and production scales. Getting the sequence wrong in your process planning can add 20–40% to unit cost and delay delivery by weeks.
This guide breaks down the real trade-offs engineers and procurement managers face when choosing between CNC machining and 금속 주조, from raw material waste to surface finish requirements. All data drawn from NADCA die casting standards, AFS sand casting specifications, and Supro MFG shop-floor records.
What Is CNC Machining in CNC Machining vs Casting?
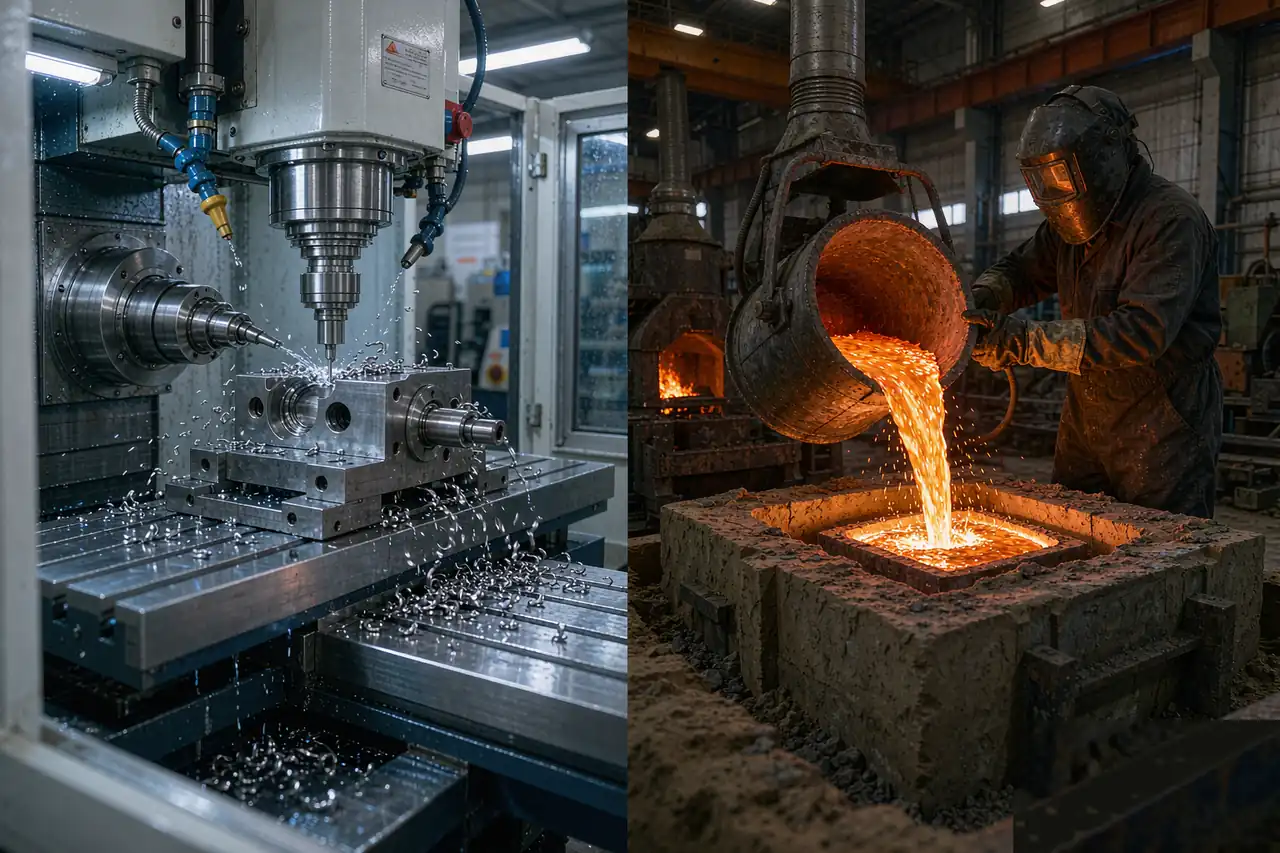
CNC (Computer Numerical Control) machining is a subtractive manufacturing process. A solid block of metal—bar stock, plate, or a pre-cast blank—is secured in a CNC mill or lathe, and multi-axis cutting tools remove material until the final geometry remains. The machine follows a digital program (G-code or CAM output) with repeatability of ±0.01 mm on good equipment.
Common CNC subtypes relevant to casting buyers:
- 3-axis milling. Entry-level; ideal for prismatic parts, pockets, and flat surfaces.
- 4/5-axis machining. Complex contours, angled holes, and aerospace-grade impellers. Tool changes and setup time increase accordingly.
- CNC turning (lathe). Rotational symmetry — shafts, housings, flanges. Often paired with casting pre-forms to reduce machinable stock.
Where Casting Fits Into CNC Planning
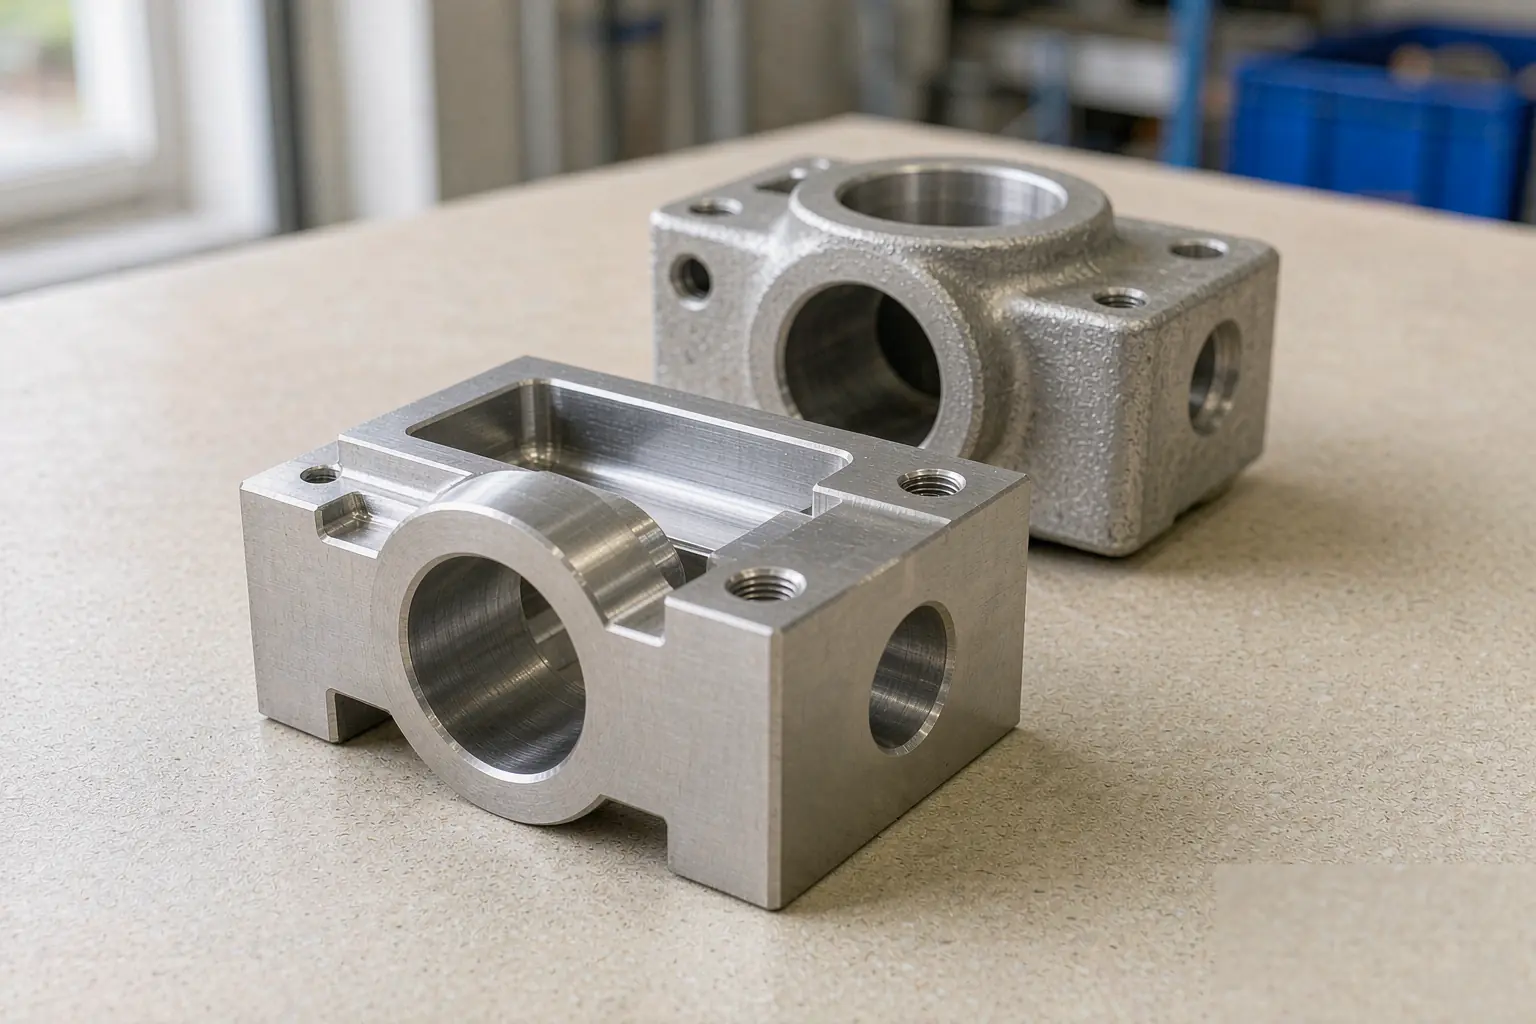
The phrase cnc machining vs casting is often a false choice. In practice, the two are sequential: casting produces the near-net-shape pre-form, and CNC machining delivers the final tolerances and surface finish. Supro MFG’s typical workflow for structural aluminum parts follows this pattern: sand casting or investment casting → CNC finish machining → inspection.
What Is Metal Casting?
Metal casting pours molten metal into a mold cavity. Once solidified, the caster ejects or breaks away the mold to extract the raw casting. Unlike CNC machining (subtractive), casting is near-net-shape—it approximates final geometry and only requires machining on features that demand tight tolerances or high surface quality.
The four casting methods most frequently compared with CNC machining for production planning:
- Sand casting. Low tooling cost, high flexibility. Suitable for pieces from 1 kg to 50 tonnes. Tolerances typically ±0.8 mm per 25 mm (ISO 8062 CT9–CT11).
- Investment casting. Wax pattern + ceramic shell. Excellent surface finish (Ra 1.6–3.2 μm), tighter tolerances than sand casting. Alloy selection spans carbon steel, stainless steel, and aluminum.
- Die casting. High-pressure injection into steel dies. Excellent dimensional repeatability, thin walls possible. Tooling is expensive ($30,000–$150,000) but justified at 10,000+ units.
- 3D printed casting patterns. Additive tooling for sand molds. Bridges prototype and production for complex geometries.
CNC Machining vs Casting: Head-to-Head Comparison
Use this table to benchmark cnc machining vs casting across the six decision factors that most affect BOM cost and delivery.
| Decision Factor | CNC 가공 | 금속 주조 |
|---|---|---|
| Unit cost (100–1,000 pcs) | $15–$80 (depends on material and complexity) | $3–$25 after tooling amortization |
| Tooling / setup cost | $500–$5,000 (fixtures, jigs, CAM programming) | $3,000–$150,000 (pattern, die, or shell) |
| Dimensional tolerance | ±0.01 mm (CNC milling); ±0.025 mm (CNC turning) | ±0.8 mm (sand); ±0.15 mm (die casting); ±0.1 mm (investment) |
| Surface finish | Ra 0.8–3.2 μm (as-machined); better with polishing | Ra 1.6–12.5 μm (as-cast); improveable by blasting or coating |
| 자재 활용도 | 60–75% (subtractive waste from bar/plate) | 85–95% (near-net; minimal excess material) |
| Lead time (first article) | 3–10 business days | 4–8 weeks (new tooling); 1–2 weeks (existing pattern) |
When CNC Machining Comes First
In certain scenarios, CNC machining is the primary—and sometimes only—manufacturing route:
- Ultra-tight tolerances below ±0.05 mm. Some aerospace and instrumentation parts exceed what any casting process can hold as-cast. CNC is non-negotiable for these features.
- Small-batch bespoke parts. When unit volume is under 20 and tooling amortization makes casting prohibitively expensive, CNC from bar stock is often the only cost-justified path.
- Parts requiring specific grain structures. Machined surfaces have predictable, consistent grain orientation. Certain fatigue-critical applications benefit from this control.
- High-alloy or exotic materials. Some nickel-based superalloys (Inconel, Hastelloy) are castable but require expensive specialty molds. CNC from rolled plate or forgings avoids these costs at low volumes.
When Casting Comes First (or Only)
Casting is the smarter primary choice when:
- Complex internal geometry. Undercuts, internal cavities, and conformal cooling channels are either impossible or prohibitively expensive in CNC. Casting (especially 3D-printed sand mold casting) handles these routinely.
- High unit volume (1,000+). Tooling cost per part drops dramatically. Die casting at 20,000 units routinely undercuts full-CNC pricing by 60–75%.
- Large or heavy parts. CNC milling a 500 kg steel housing from a 700 kg forging or plate is material-inefficient and slow. Casting handles large geometries with far less waste.
- Alloy flexibility needed. When selecting the right casting alloy for corrosion resistance or high-temperature performance, casting opens access to a wider range of compositions than most machined stock materials.
The Casting-First Defect Risk to Plan For
When casting precedes CNC, be aware that 주조 결함 (porosity, shrinkage, cold shuts) may hide inside the pre-form and only become apparent after CNC machining reveals them. A 100% X-ray or DPIT inspection on the raw casting before machining is standard practice for safety-critical applications—factor this into your process planning and cost estimate.
Decision Framework: CNC First or Casting First?
Apply this three-question filter to decide the production sequence:
- Q1 — Tolerance check. Are any critical features tighter than ±0.15 mm? If yes → those features will be CNC-machined regardless. Can the casting hold tolerances on the non-critical features? If yes → casting-first with CNC finish.
- Q2 — Volume check. Is the production run over 5,000 units? If yes → die casting or permanent mold with CNC finish is almost always cheaper. Under 500 units → sand casting or CNC from bar stock depending on complexity.
- Q3 — Geometry check. Does the part have internal passages, conformal cooling channels, or heavy undercuts? If yes → casting is almost certainly the right primary process. If the geometry is a simple prism → CNC from plate may be faster and cheaper even at mid-volume.
자주 묻는 질문
Can I use CNC machining instead of casting for all my parts?
Technically yes, but economically no for most production volumes above 100 units with complex geometry. CNC waste from bar stock can account for 25–40% of raw material cost—and for large parts, machining time becomes prohibitive. For B2B buyers optimizing cost-per-part, the cnc machining vs casting decision should always factor in total BOM cost, not just unit machining time.
What is the typical tolerance for sand casting before CNC finishing?
Standard sand casting delivers CT9–CT11 tolerances per ISO 8062 (±0.8 mm to ±1.6 mm per 25 mm). Investment casting improves this to CT5–CT7 (±0.1–0.2 mm). All features requiring tighter tolerances are CNC-machined as a secondary operation. Working with a metal casting supplier who engineers the machining allowance upfront avoids costly re-work.
How do I reduce lead time when my project needs both casting and CNC?
Three strategies: (1) use existing casting patterns (eliminates tooling lead time of 4–8 weeks); (2) parallelize the casting cure and CNC programming phases rather than sequencing them; (3) for prototype quantities, consider 3D-printed sand molds via 3D printed casting patterns to reduce tooling to days rather than weeks.
Is die casting always better than sand casting when volume is high?
Not always. Die casting requires expensive steel tooling ($30,000–$150,000) and is best suited for aluminum, zinc, and magnesium alloys. For steel or iron parts at high volumes, the tooling cost and cycle time make sand casting or centrifugal casting more economical. The sand casting vs investment casting comparison also applies—each process has its sweet spot by alloy and geometry.
*Tolerances referenced from ISO 8062 (casting tolerances) and NADCA 2015 (die casting). Unit cost ranges reflect 2025 B2B market data for aluminum and carbon steel. Supro MFG provides both CNC machining and metal casting services with in-house quality inspection (X-ray, DPIT, CMM).
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina