
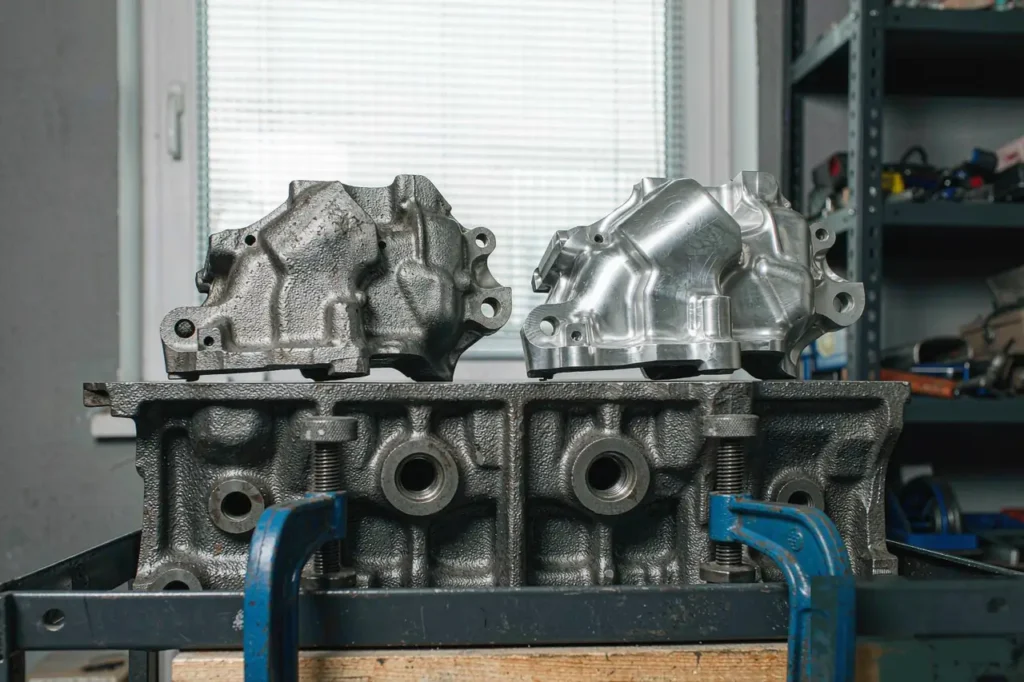
For B2B buyers, acabado de superficies de fundición is rarely a cosmetic afterthought — it dictates paint adhesion, sealing performance, fatigue life, and whether a part passes a 100% visual inspection at incoming quality control. A 1.6 µm Ra on an as-cast aluminum housing versus a 6.3 µm Ra often decides if the downstream coater has to bead-blast anyway, and who pays for the rework.
This guide walks shop-floor buyers and design engineers through the acabado de superficies de fundición options that actually hold up in production: mechanical blasting, hand and robotic polishing, conversion coatings, and paint or powder systems. Real numbers come from AFS Casting Source Directory finishing reference data and shop-floor records at Supro MFG.
Why Casting Surface Finishing Is a Sourcing Decision, Not a Final Step
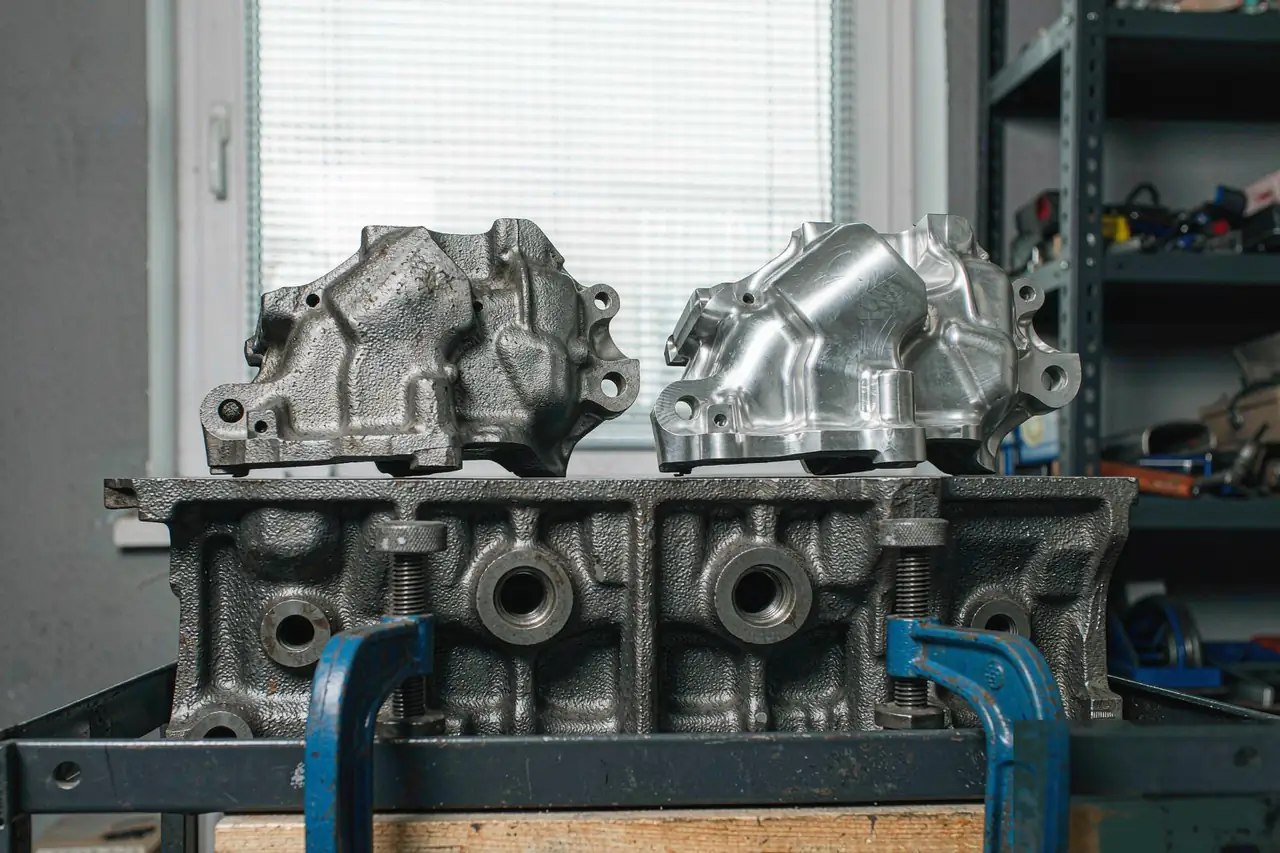
Roughness, draft marks, micro-shrinkage, and oxide scale all ride along on the raw casting. If you wait until defectos comunes en la fundición show up at the customer site to address surface quality, you have already paid for the wrong process. Procurement teams that lock finishing grade, blasting media, and coating spec into the acabado de superficies de fundición RFQ up-front typically avoid two rounds of part rejection.
- Functional surfaces — bearing bores, seal lands, hydraulic spools — usually require 0.8–1.6 µm Ra and a defined lay pattern.
- Painted or coated cosmetic surfaces generally need 3.2–6.3 µm Ra to give the coating mechanical anchor.
- As-shipped raw surfaces for industrial housings can ride at 6.3–12.5 µm Ra if the spec allows oil or wax protection.
Mechanical Surface Preparation: Blasting, Grinding, and Polishing
Most acabado de superficies de fundición lines start with mechanical prep. The choice depends on substrate hardness, the geometry of the part, and what the next operation is.
Shot and bead blasting
Steel shot at 0.4–0.8 mm cuts a peened profile of 3.2–6.3 µm Ra on iron and steel castings, while glass bead at 100–200 µm gives aluminum castings a smoother 1.6–3.2 µm Ra satin finish. Coverage of 100–120% of the surface area is the typical shop standard; below that, residual oxide pulls paint adhesion down by roughly 30%. For critical aluminum housings in our shop, bead blasting also acts as a light sand casting surface refinement step before conversion coating.
Hand and robotic grinding
Grinding is reserved for parting-line flash, sprue stubs, and riser contacts. A standard 60-grit ceramic disc removes roughly 0.2–0.4 mm per pass on gray iron; switching to 120-grit drops material removal to 0.05 mm per pass and leaves a finish suitable for direct paint. Robotic grinding is now standard on volume runs above 5,000 pieces per month where the cycle time is steady.
Polishing and buffing
Mirror finishes under 0.4 µm Ra only make sense on stainless investment castings used for sanitary or food-grade applications. The cost is real: an experienced polisher handles 8–12 small parts per hour, and a robotic cell runs 50–80 parts per hour with a 10–15% rework rate on first article. We generally recommend polishing only after alloy selection and gating design have been frozen.
| Método | Typical Ra range | Best substrate | Cost driver |
|---|---|---|---|
| Steel shot blasting | 3.2–6.3 µm | Iron & steel | Media wear |
| Glass bead blasting | 1.6–3.2 µm | Aluminum, zinc | Bead cost |
| Robotic grinding | 1.6–4.0 µm | Any cast metal | Cell capex |
| Manual polishing | 0.2–0.8 µm | Stainless, brass | Labor hours |
Chemical and Conversion Coatings Before Paint
After mechanical prep, most ferrous and aluminum castings get a conversion layer. The right chemistry depends on whether the part lives indoors, outdoors, or under a vehicle.
- Iron phosphate (Fe-Ph) on steel and iron — coating weight 1.0–2.5 g/m², paint adhesion rated 4B–5B on ASTM D3359 cross-hatch. Suited to indoor and under-hood duty.
- Zinc phosphate (Zn-Ph) on steel — coating weight 1.5–3.0 g/m², paired with a seal rinse for salt-spray life beyond 500 hours ASTM B117.
- Chromate conversion on aluminum per MIL-DTL-5541, classes 1A and 3 — used as a paint base or as a standalone corrosion layer for indoor service.
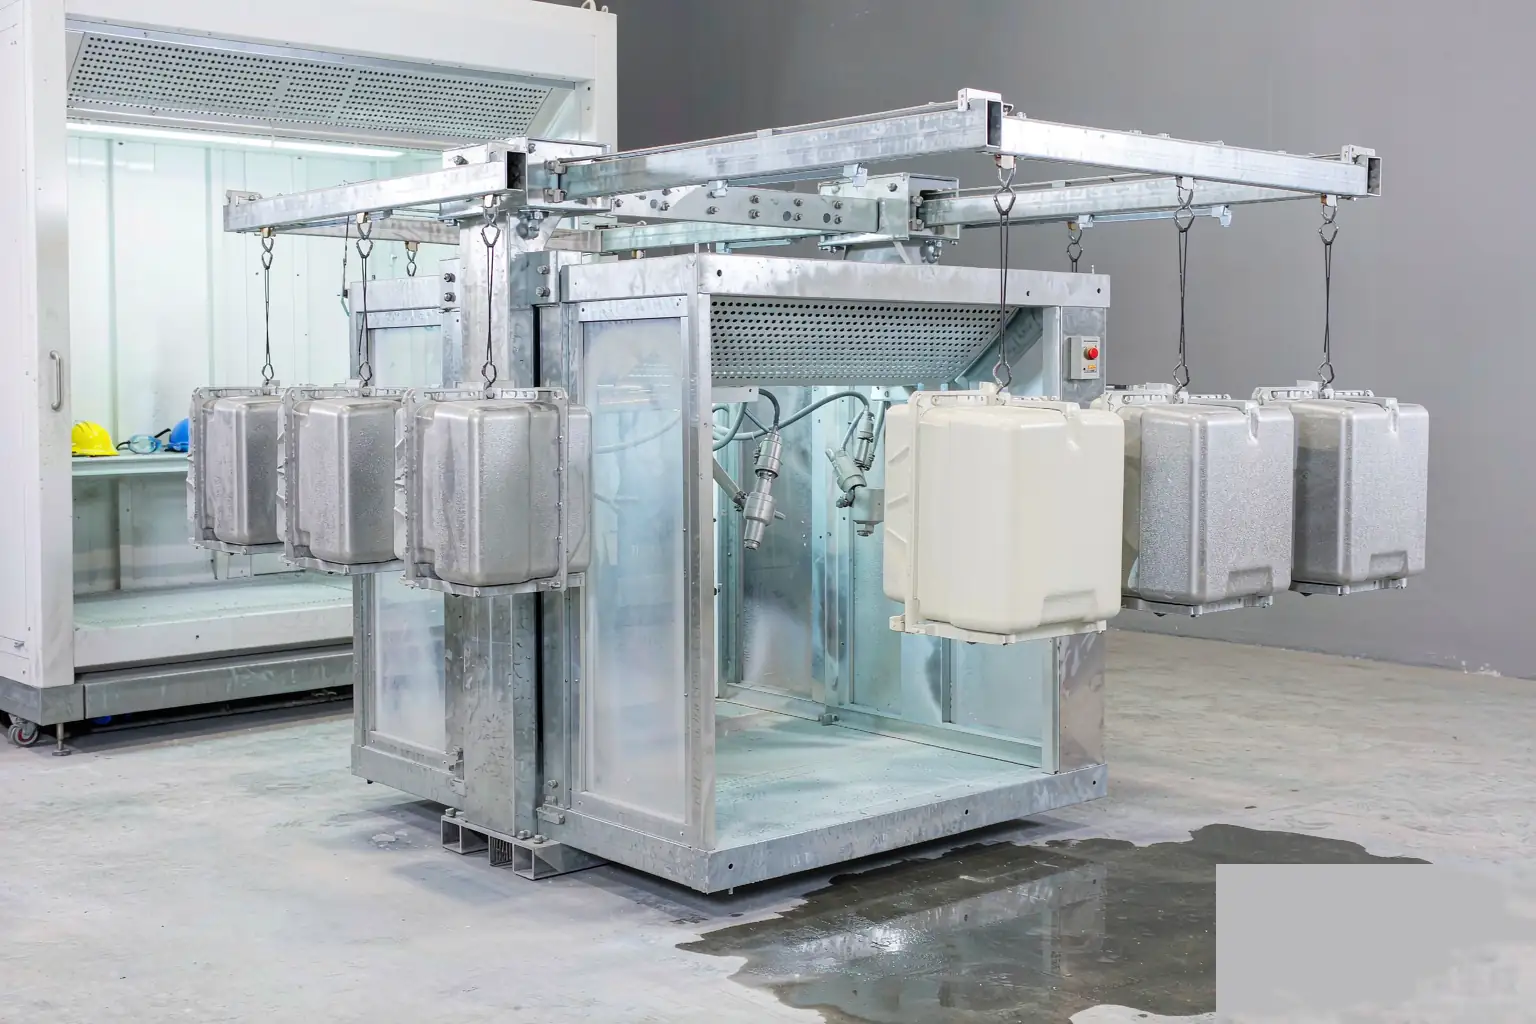
Outdoor and under-chassis parts step up to zinc-rich primer, epoxy mid-coat, and a top coat, or to powder coating at 60–80 µm DFT. Our field data on underbody brackets shows that an e-coat plus powder top-coat extends resistencia a la corrosión past 1,000 hours ASTM B117 versus roughly 240 hours for liquid paint alone.
How Casting Surface Finishing Fits the Wider Process Chain
Surface finish is the end of a chain that started with alloy pour and mold design. Iron-rich skins on ductile iron, oxide entrapment on aluminum fundición de metales pours, and microporosity on investment castings all translate into surface defects that finishing cannot fully hide — only mask. The cleanest acabado de superficies de fundición outcomes we ship come from parts where the upstream casting process selection, tratamiento térmico, and finishing spec were agreed before tooling cut.
If you are scoping an RFQ, a useful order is: define the Ra range and visual standard → pick the blasting or grinding method → lock the conversion coating and paint system → only then commit to a finishing partner. Reversing that order tends to add 20–35% to the per-part finishing cost on the first three production lots.
Preguntas frecuentes
What Ra range should I specify for a painted iron casting?
A 3.2–6.3 µm Ra is the practical sweet spot for painted iron castings. Below 1.6 µm Ra the paint anchor is too shallow; above 12.5 µm Ra the profile peaks show through the top coat.
Can I skip blasting if the casting already looks smooth?
No — visible smoothness does not equal coating-ready surface. A light bead or shot blast at 100% coverage is the cheapest insurance against paint delamination, even on cosmetic surfaces.
How long does a conversion coating plus powder top coat last outdoors?
A zinc phosphate plus polyester powder top coat at 60–80 µm DFT typically reaches 1,000+ hours ASTM B117 salt spray. Marine or de-icing salt duty needs a zinc-rich primer plus epoxy, or a duplex zinc-flake system.
Does finishing cost more than the casting itself?
On complex, precision-grade parts, finishing and inspection together can run 30–60% of the total part cost. Locking the spec early is the strongest lever to keep that share in the lower end of the range.
*Data referenced from AFS Casting Source Directory and Supro MFG shop-floor records.
 English
 Français
 Deutsch
 Italiano
 日本語
 한국어
 Polski
 Português de Angola
 Русский
 Español de Argentina